Explore our world-class inventory engineered with high-precision components, strict CE compliance, and reliable 5+ year warranties for advanced clinical operations worldwide.
Deep-dive technical analysis addressing semantic intent, supply chain agility, and rigorous compliance standards across international medical markets.
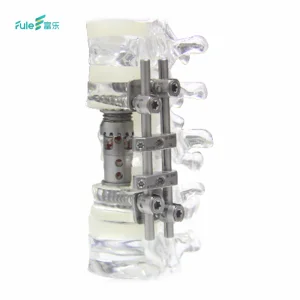
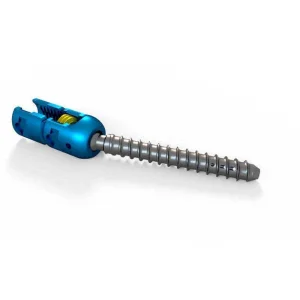
In modern healthcare paradigms, the intersection of portable diagnostic imaging systems and high-precision orthopedic implants has redefined patient outcomes. As a premier manufacturer and exporter rooted in China's robust industrial landscape, we bridge the gap between advanced engineering and clinical utility. Portable imaging devices—ranging from compact fluoroscopy units to high-resolution mobile C-arms—demand seamless synergy with spinal systems, fusion cages, and pedicle screw assemblies. This whitepaper analyzes the structural dynamics of global medical procurement, highlighting how technical rigor and robust supply chains empower international healthcare providers.
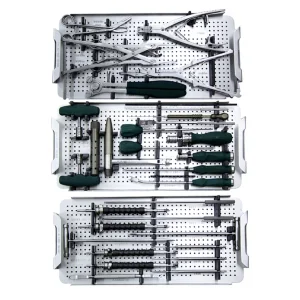
Portable medical technologies are no longer confined to traditional metropolitan hospital suites. Across diverse geographies—from emergency trauma response units in Southeast Asia to remote orthopedic clinics in Eastern Europe—portable imaging devices provide immediate, life-saving diagnostics. When paired with our CE-certified titanium spinal instruments and micro-invasive fusion cages, surgeons can execute complex spinal realignments in resource-constrained environments without compromising safety or structural precision.
The next decade of medical device manufacturing will be dictated by AI-driven imaging enhancement, lightweight alloy metallurgy, and IoT-enabled asset tracking. Our R&D division—comprising 20 dedicated graduate engineers—is continuously iterating on smart implant designs and low-profile fixation systems. By integrating predictive analytics into manufacturing workflows, we ensure that every export batch meets zero-defect thresholds, establishing benchmarks for durability and biocompatibility.
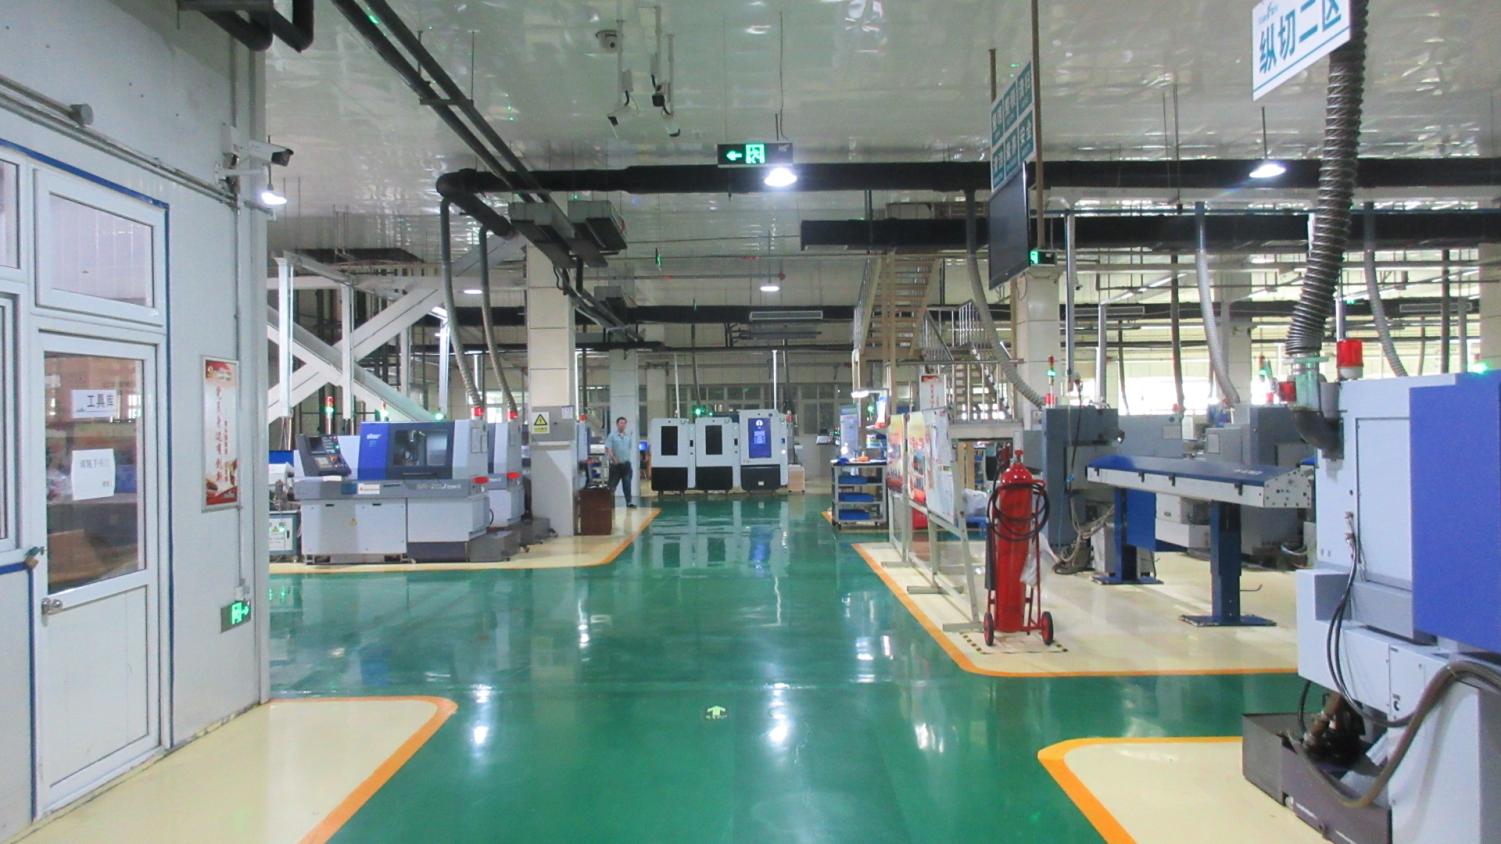
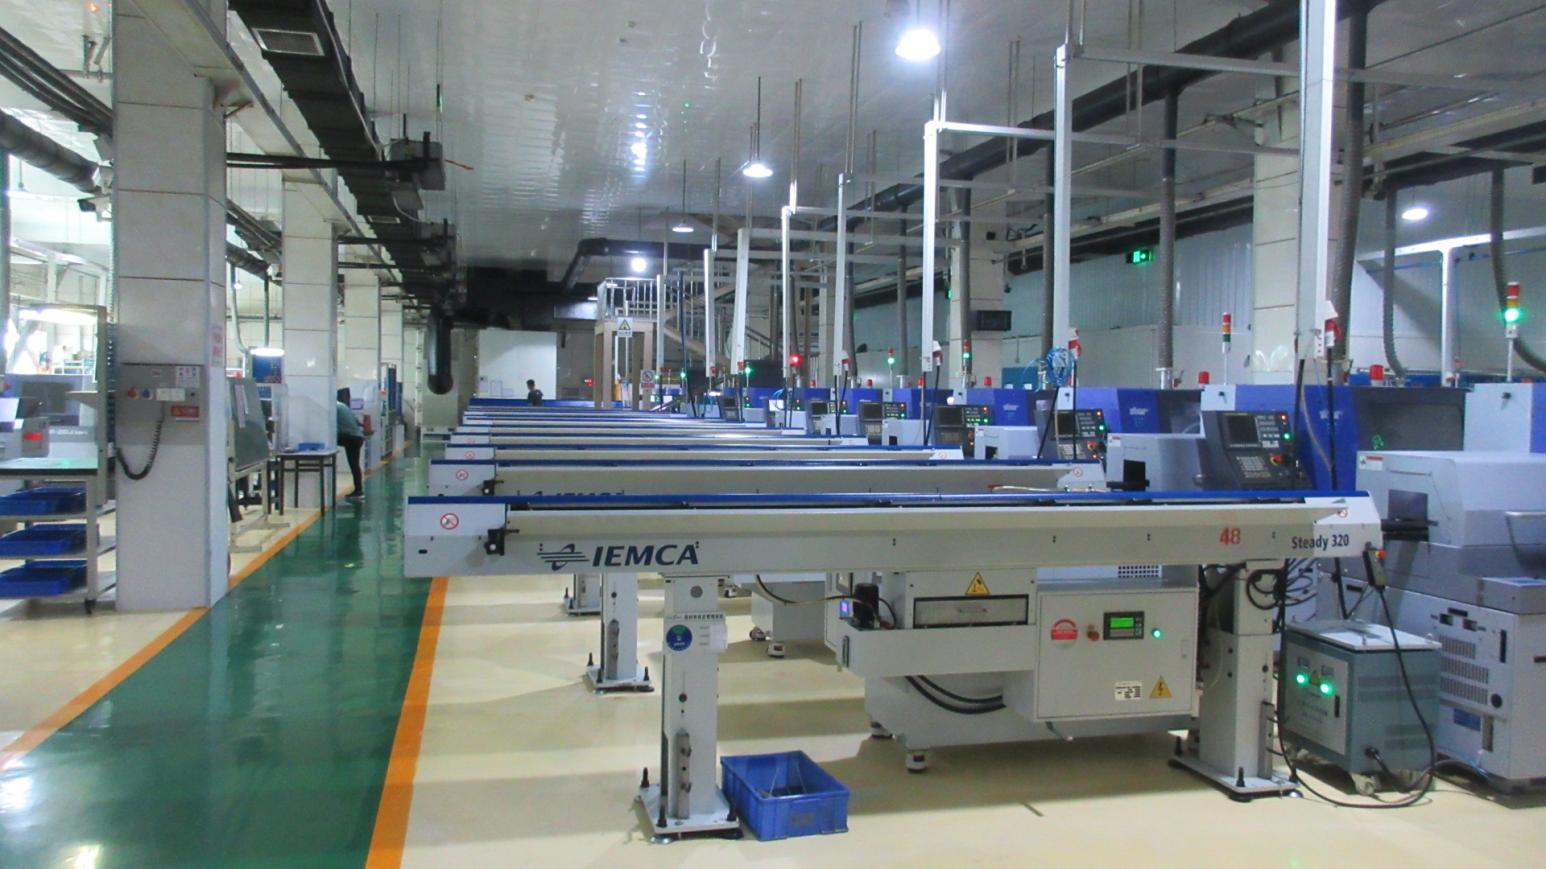
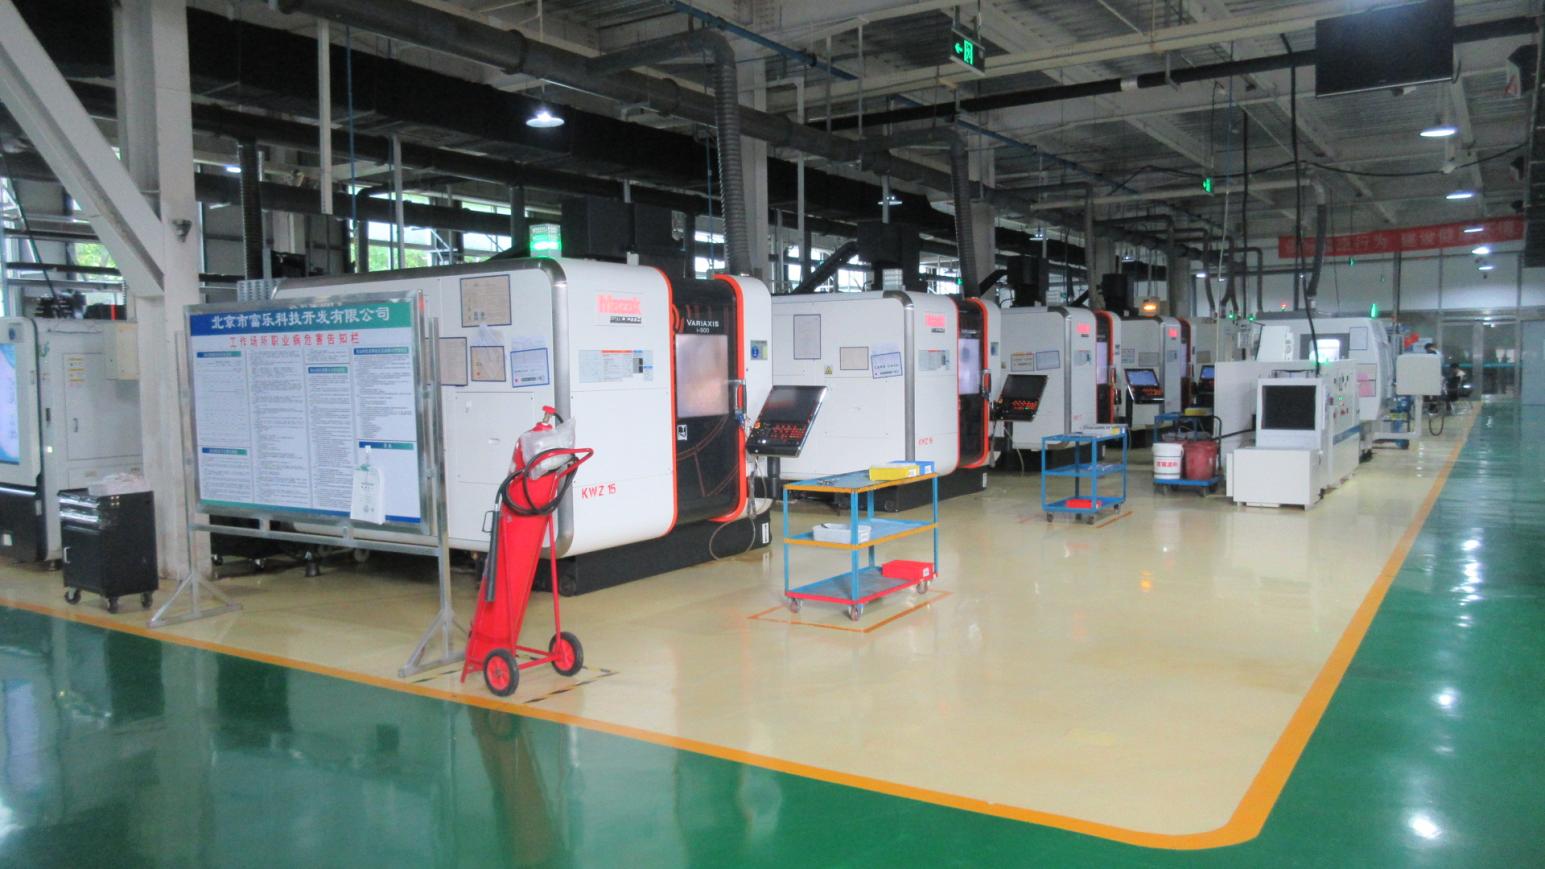
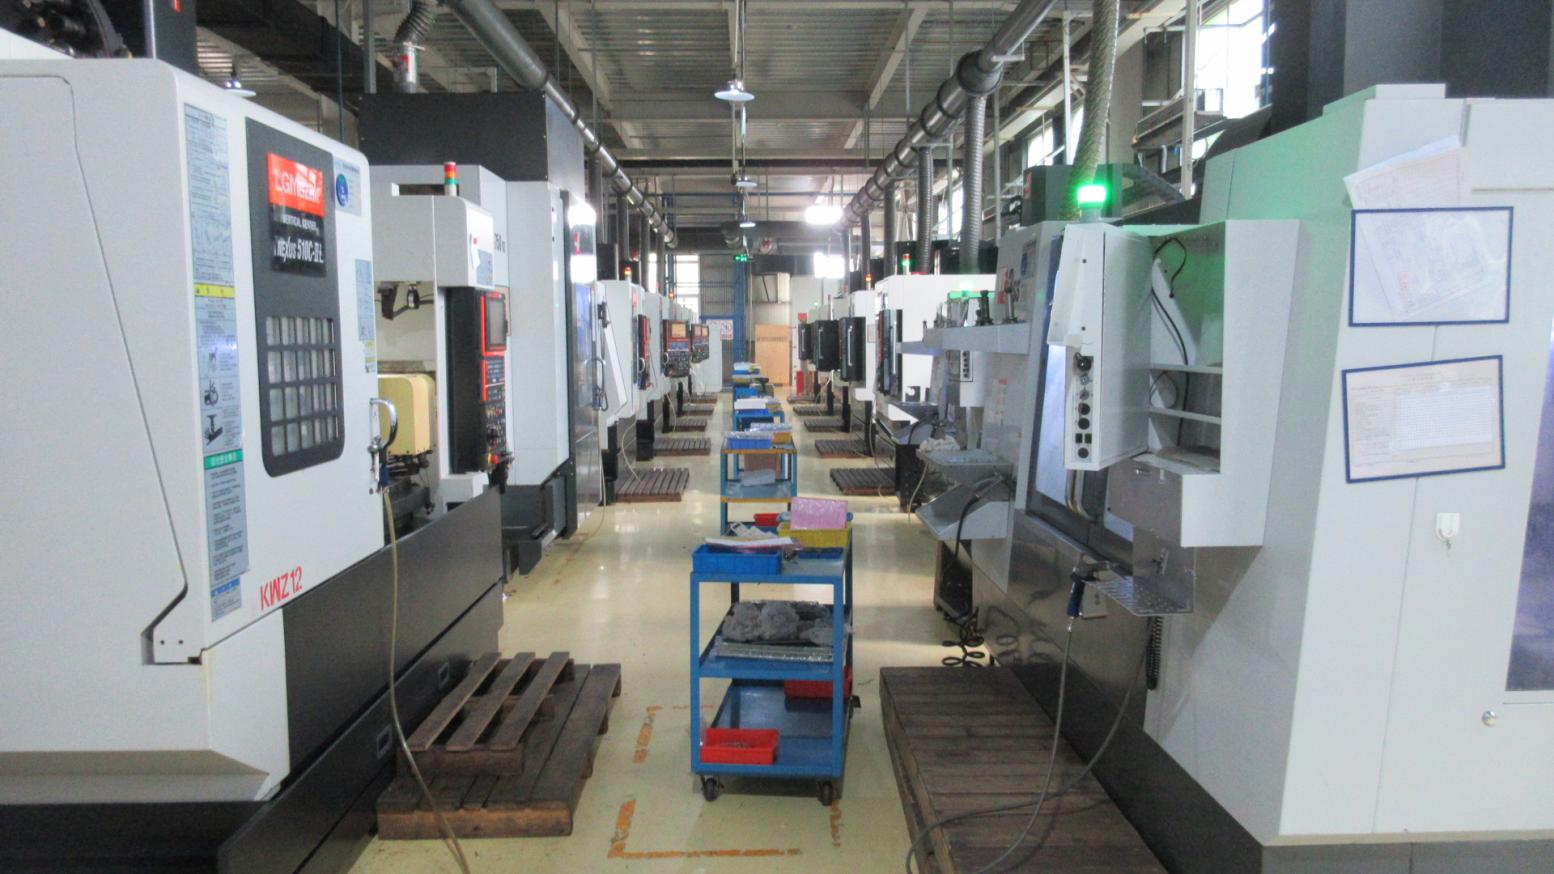
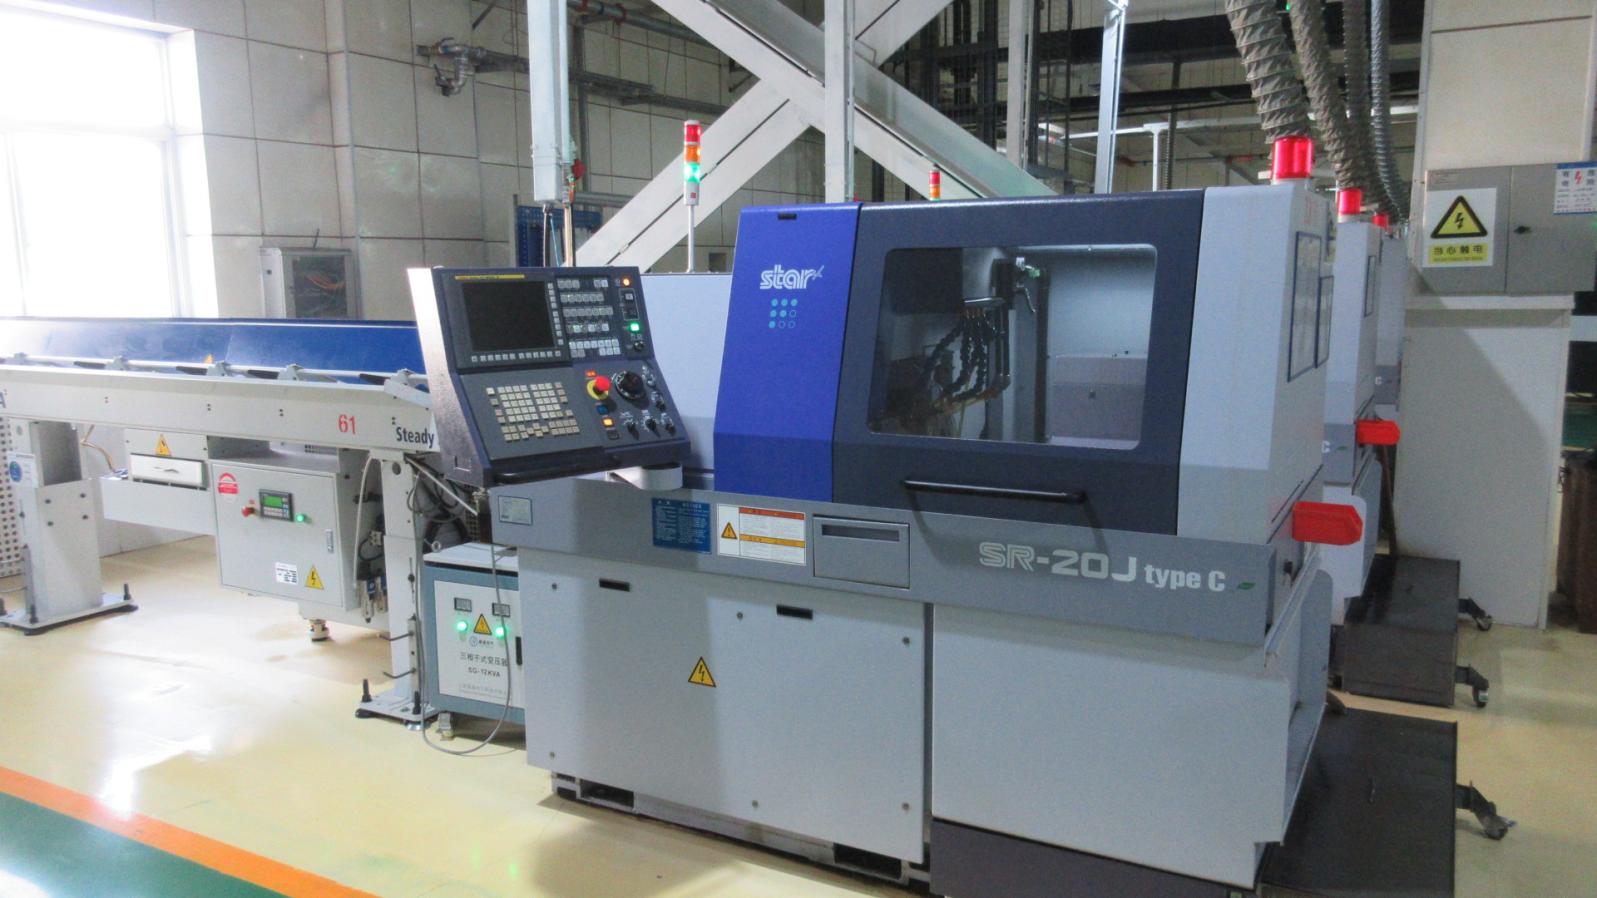
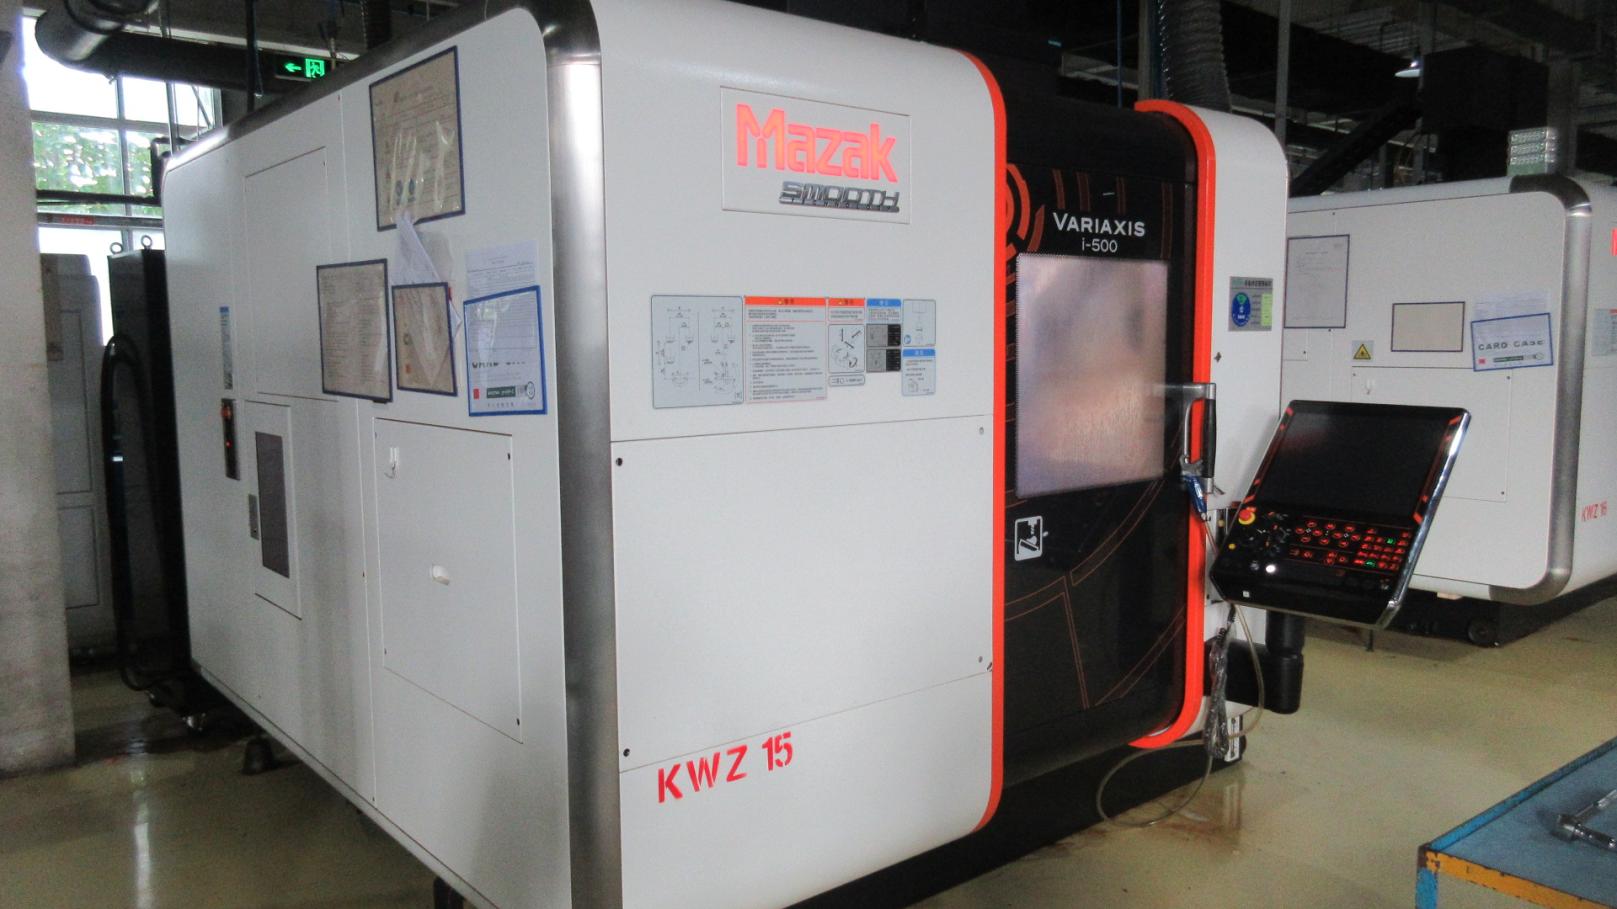
Operating a sprawling 10,000-square-meter production facility backed by 29 years of industry mastery, our enterprise exemplifies China's unmatched manufacturing resilience. Leveraging 102 state-of-the-art production machines and an annual output capacity exceeding 508,000 units, we maintain complete control over raw material traceability and tier-1 supplier partnerships. This structural independence shields international buyers from global supply chain volatility, ensuring predictable lead times and highly competitive wholesale pricing.
Measurable indicators reflecting our robust manufacturing infrastructure, strict quality control protocols, and global market reach.
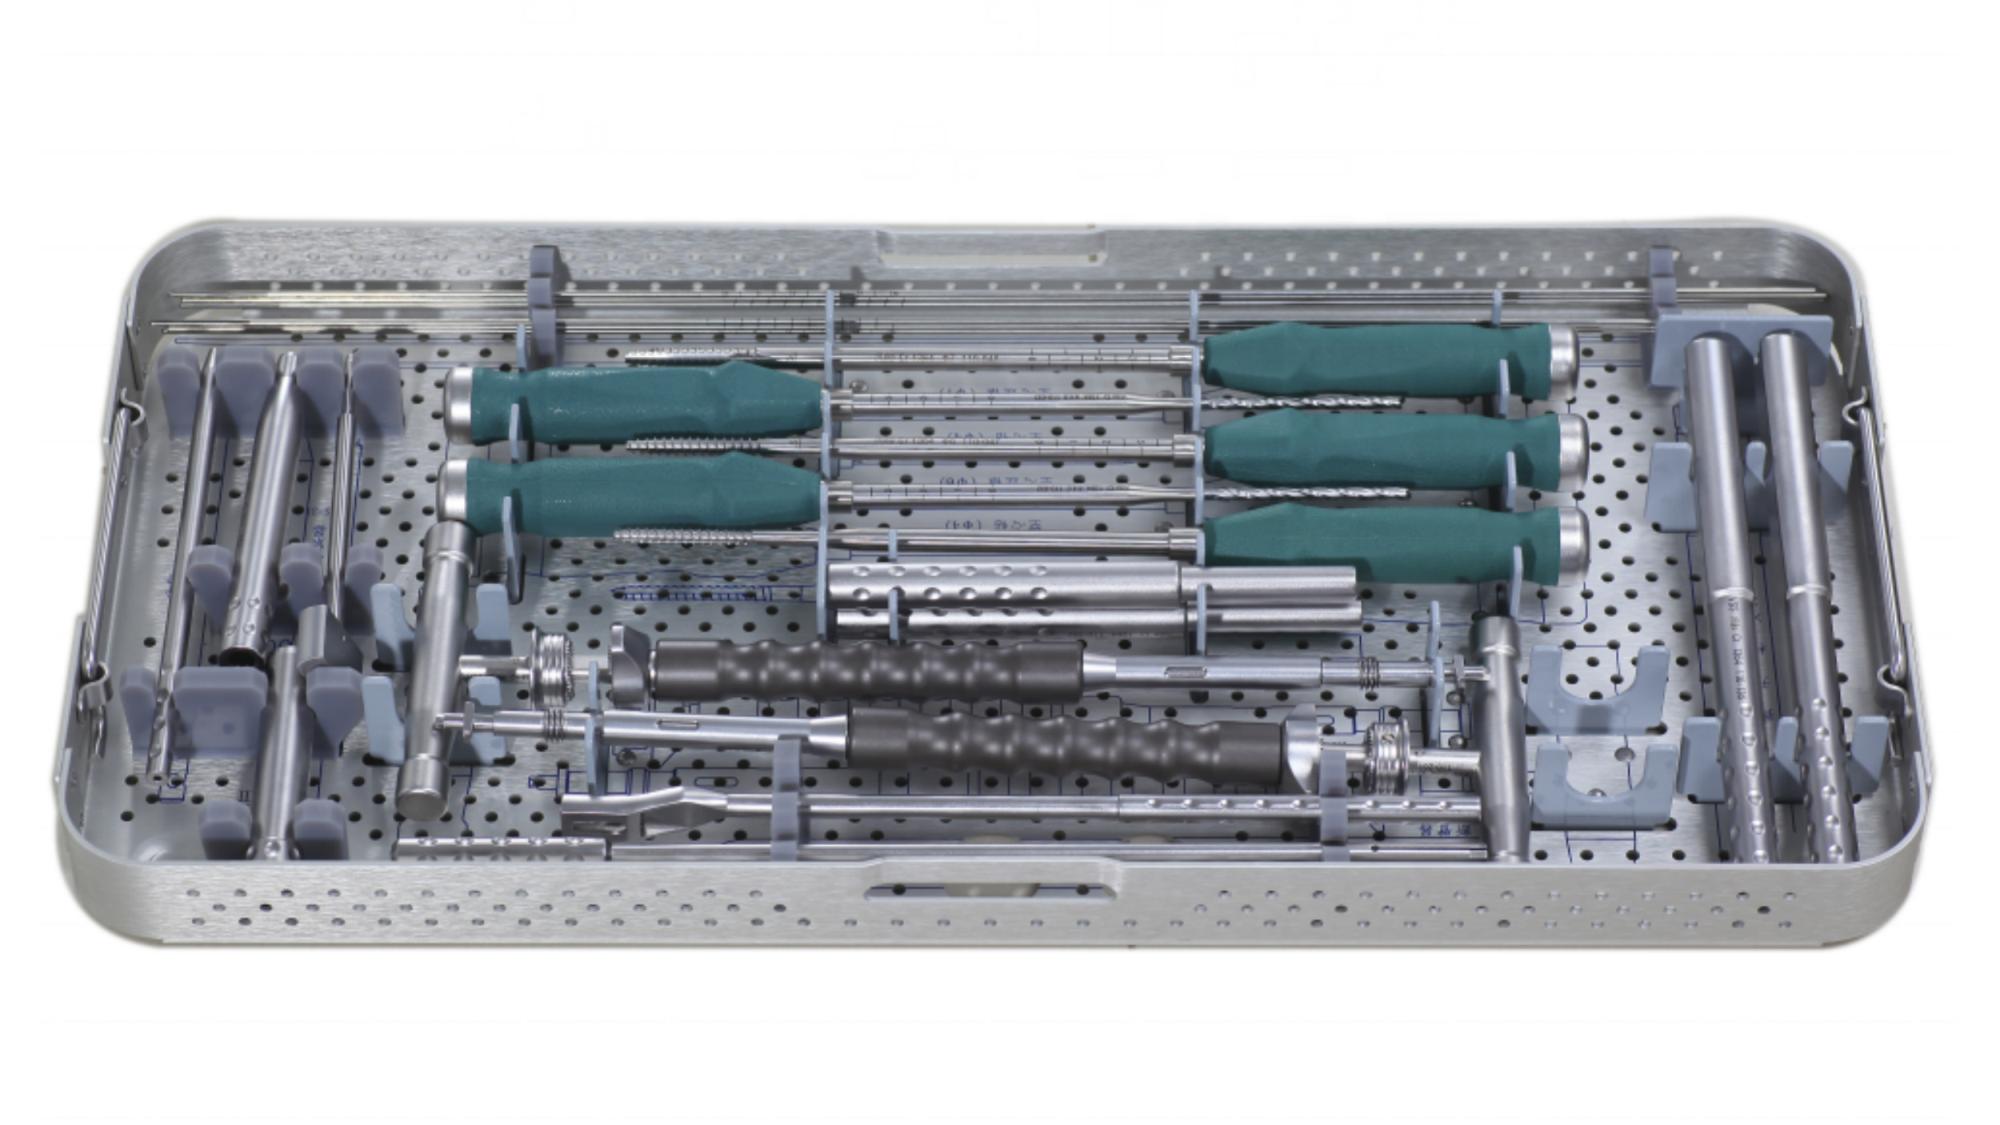
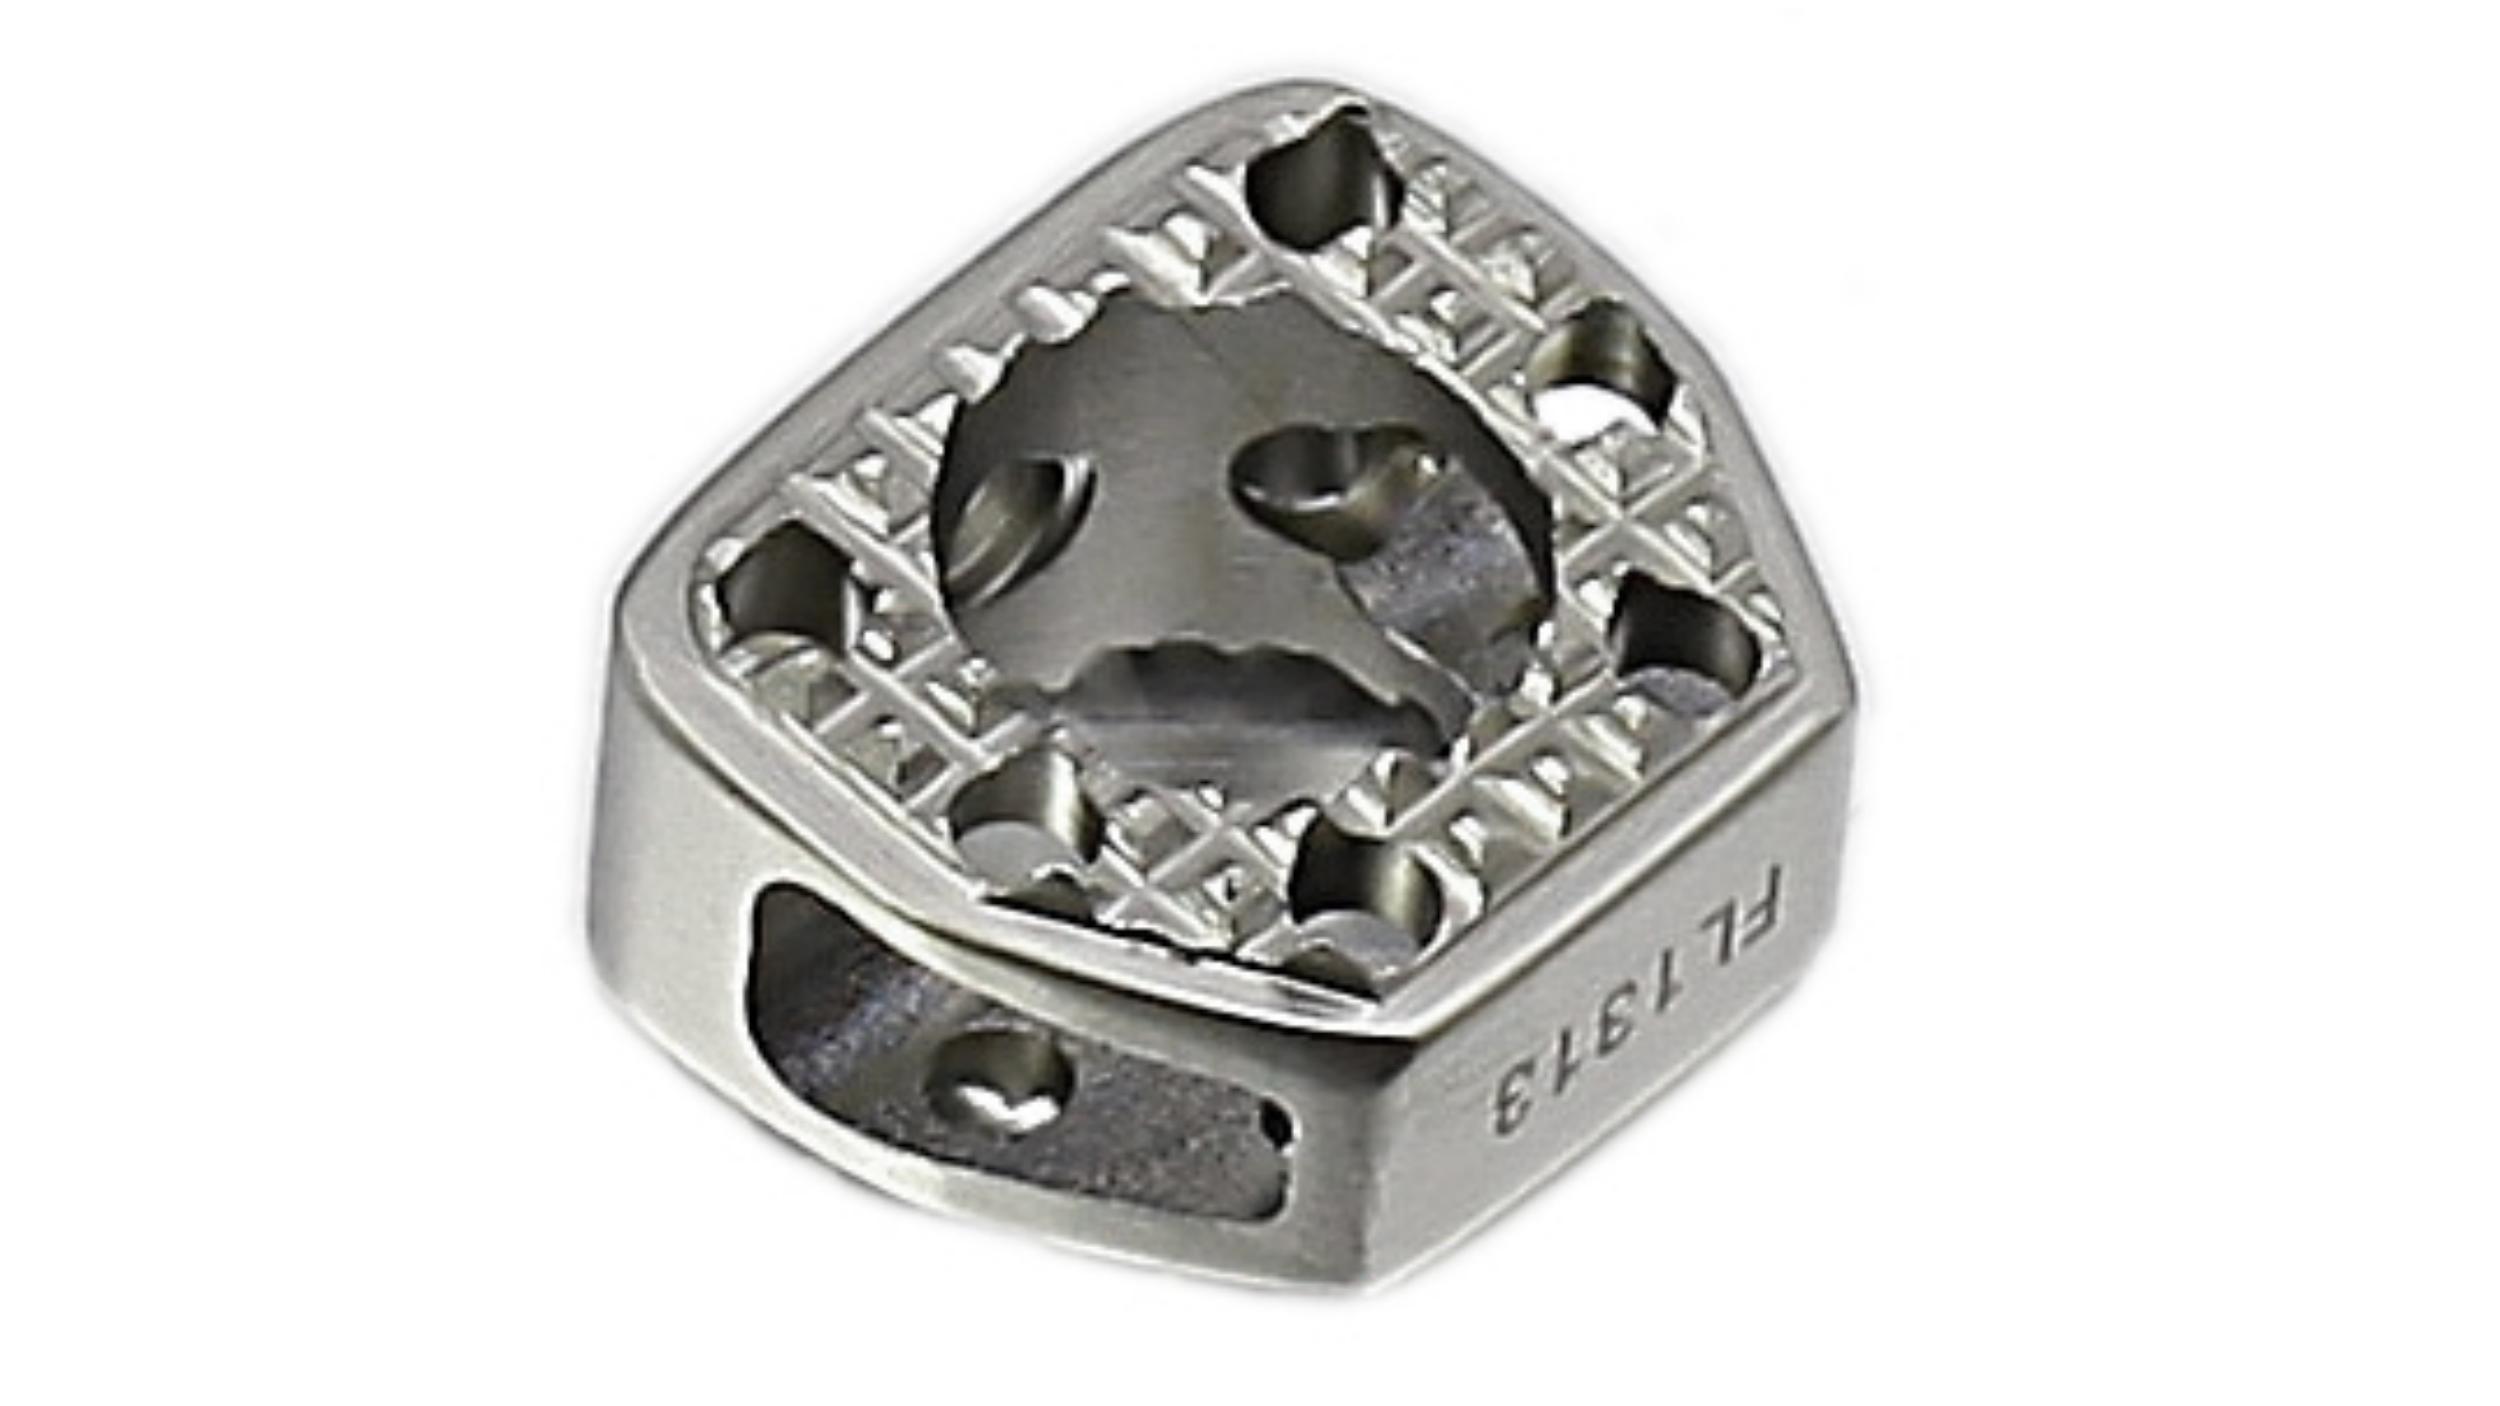
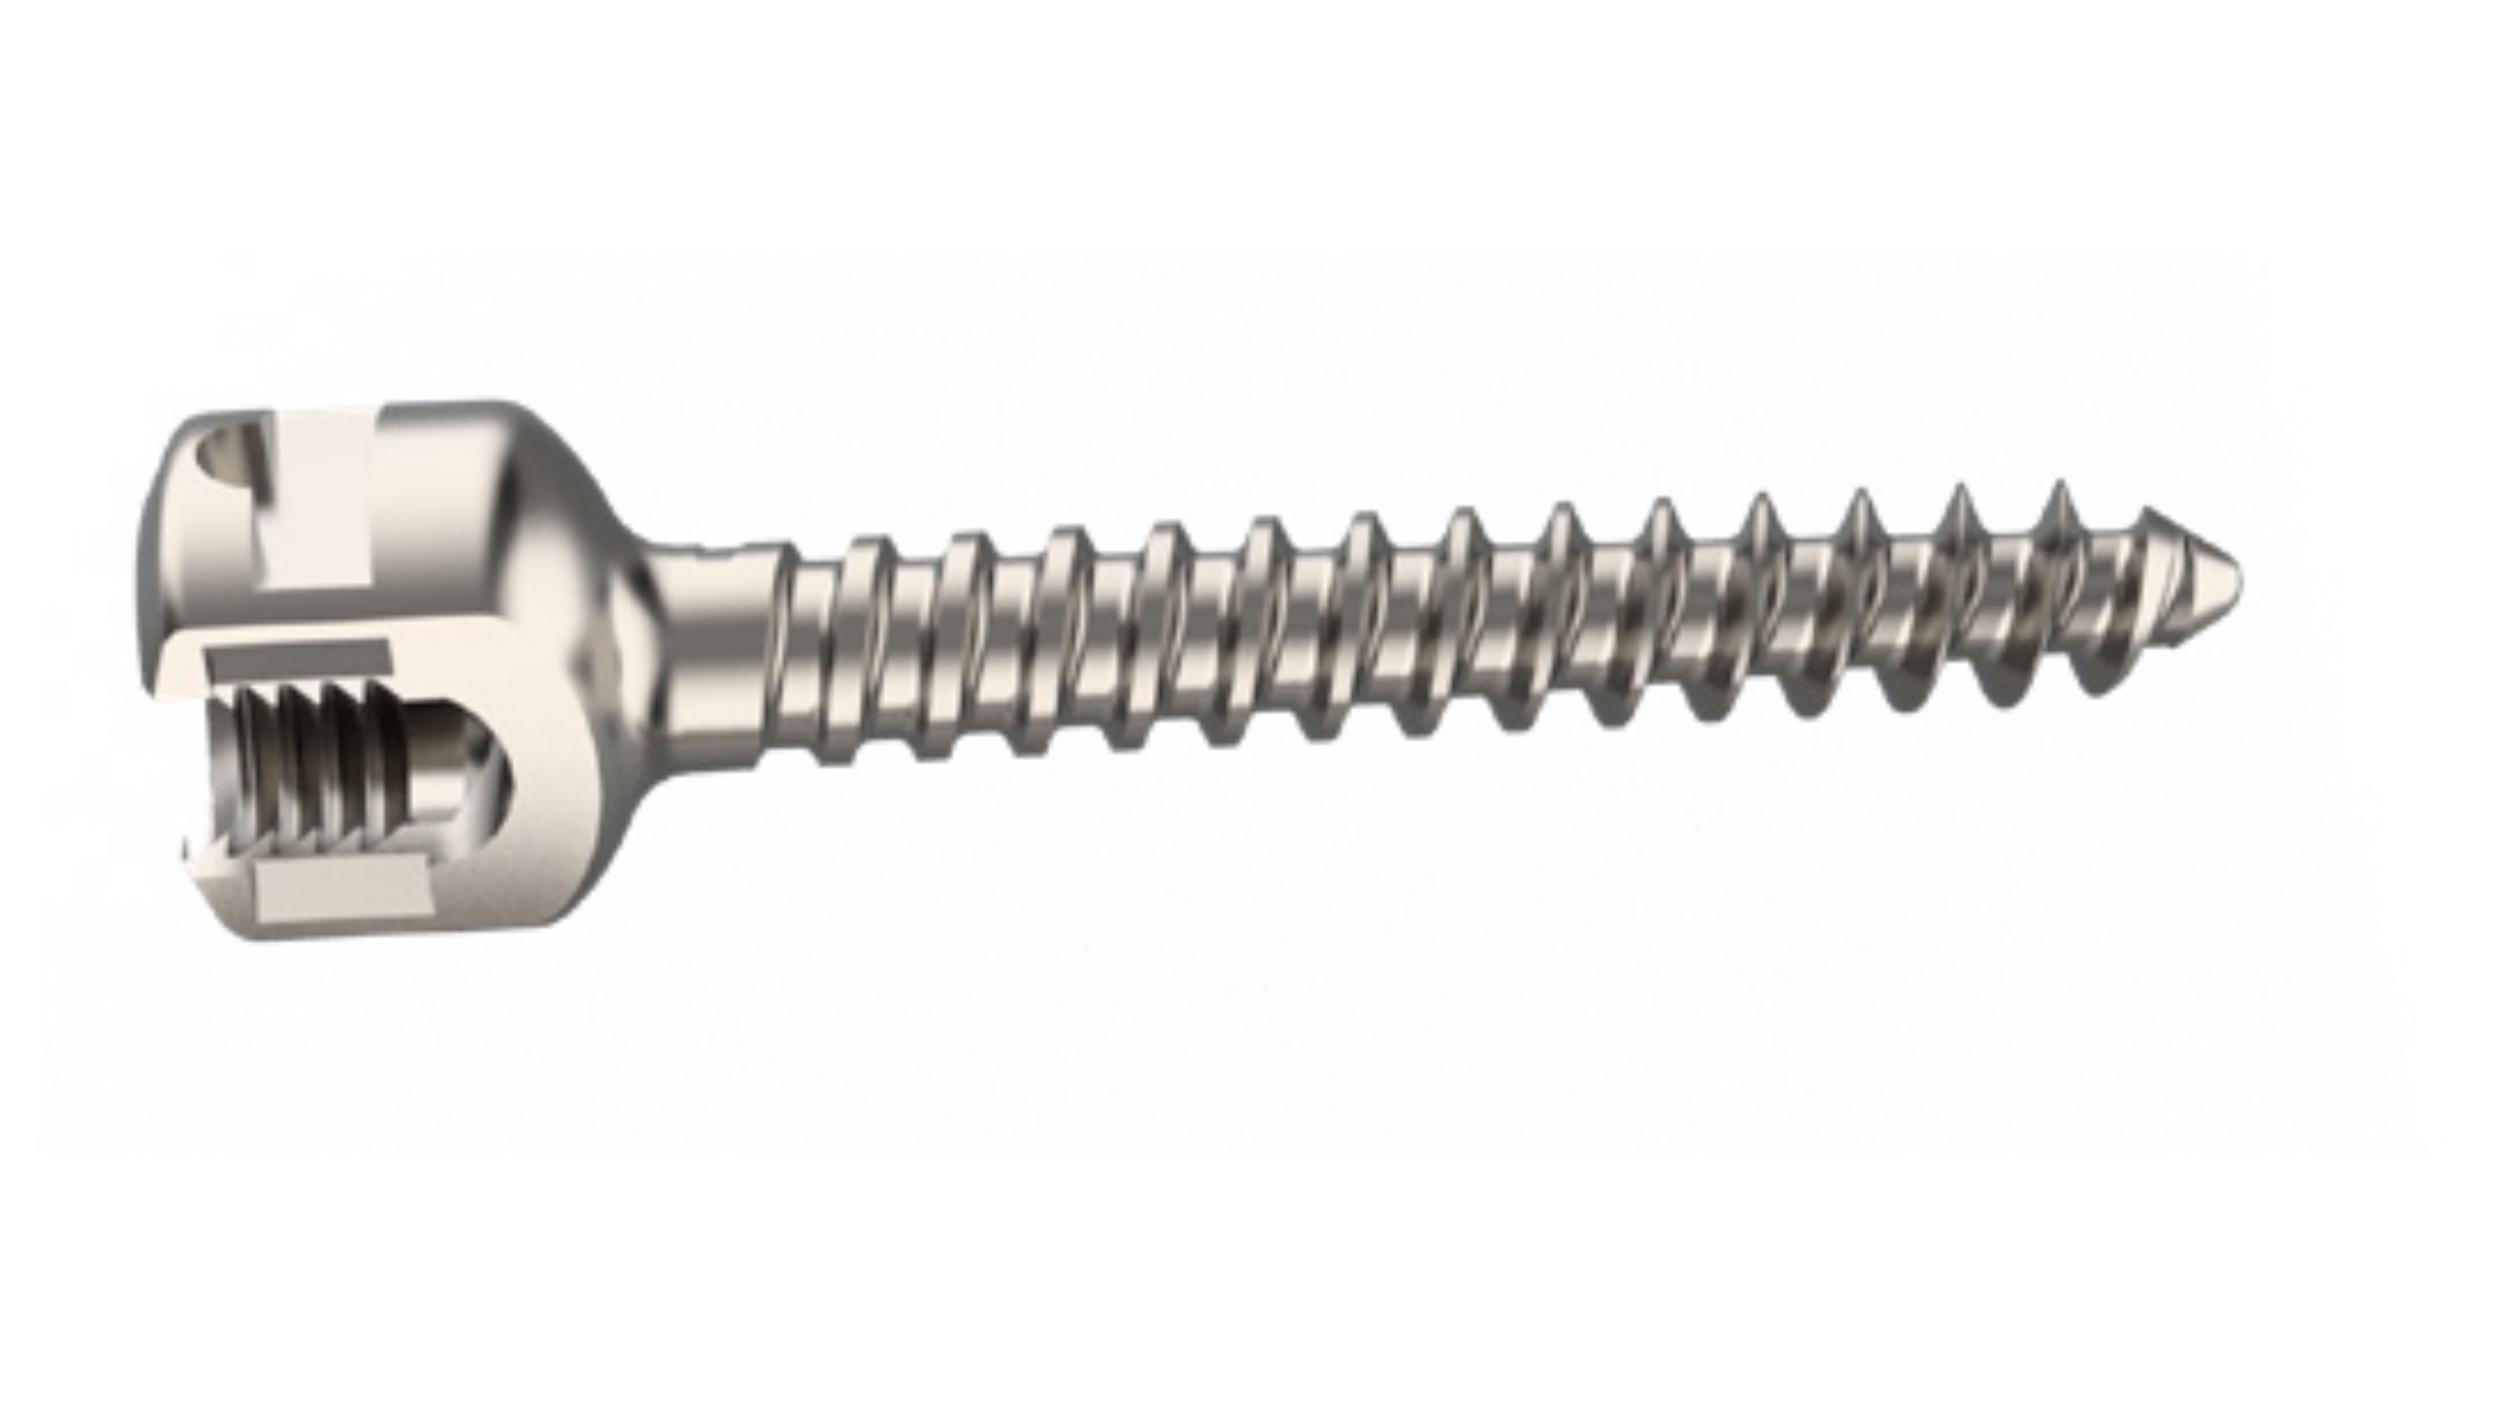
Continuing our comprehensive portfolio of CE-certified titanium medical solutions designed for superior biomechanical stability.
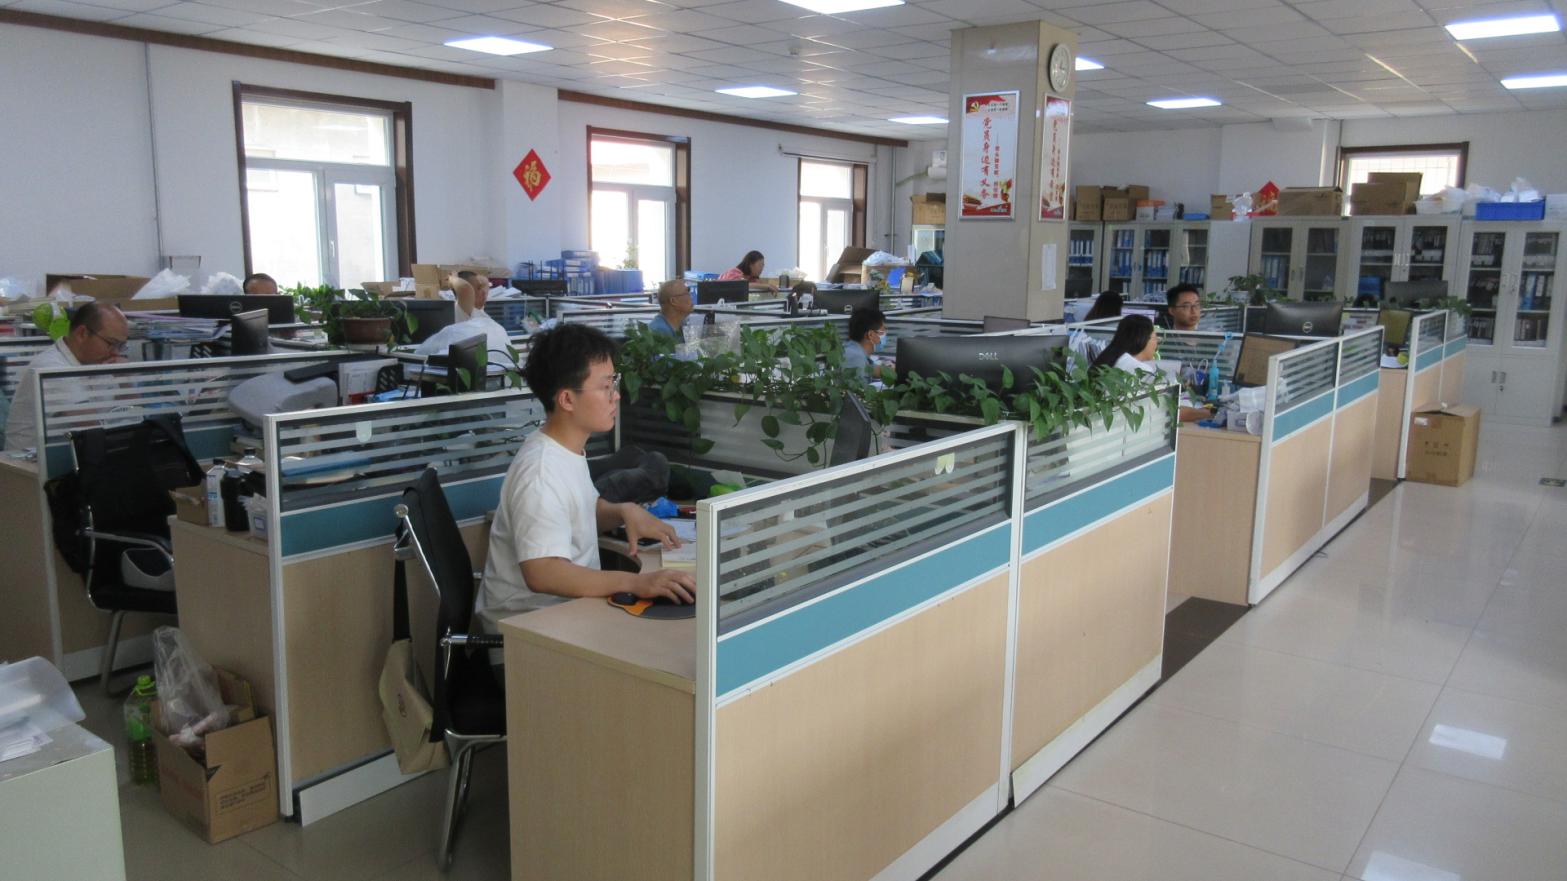
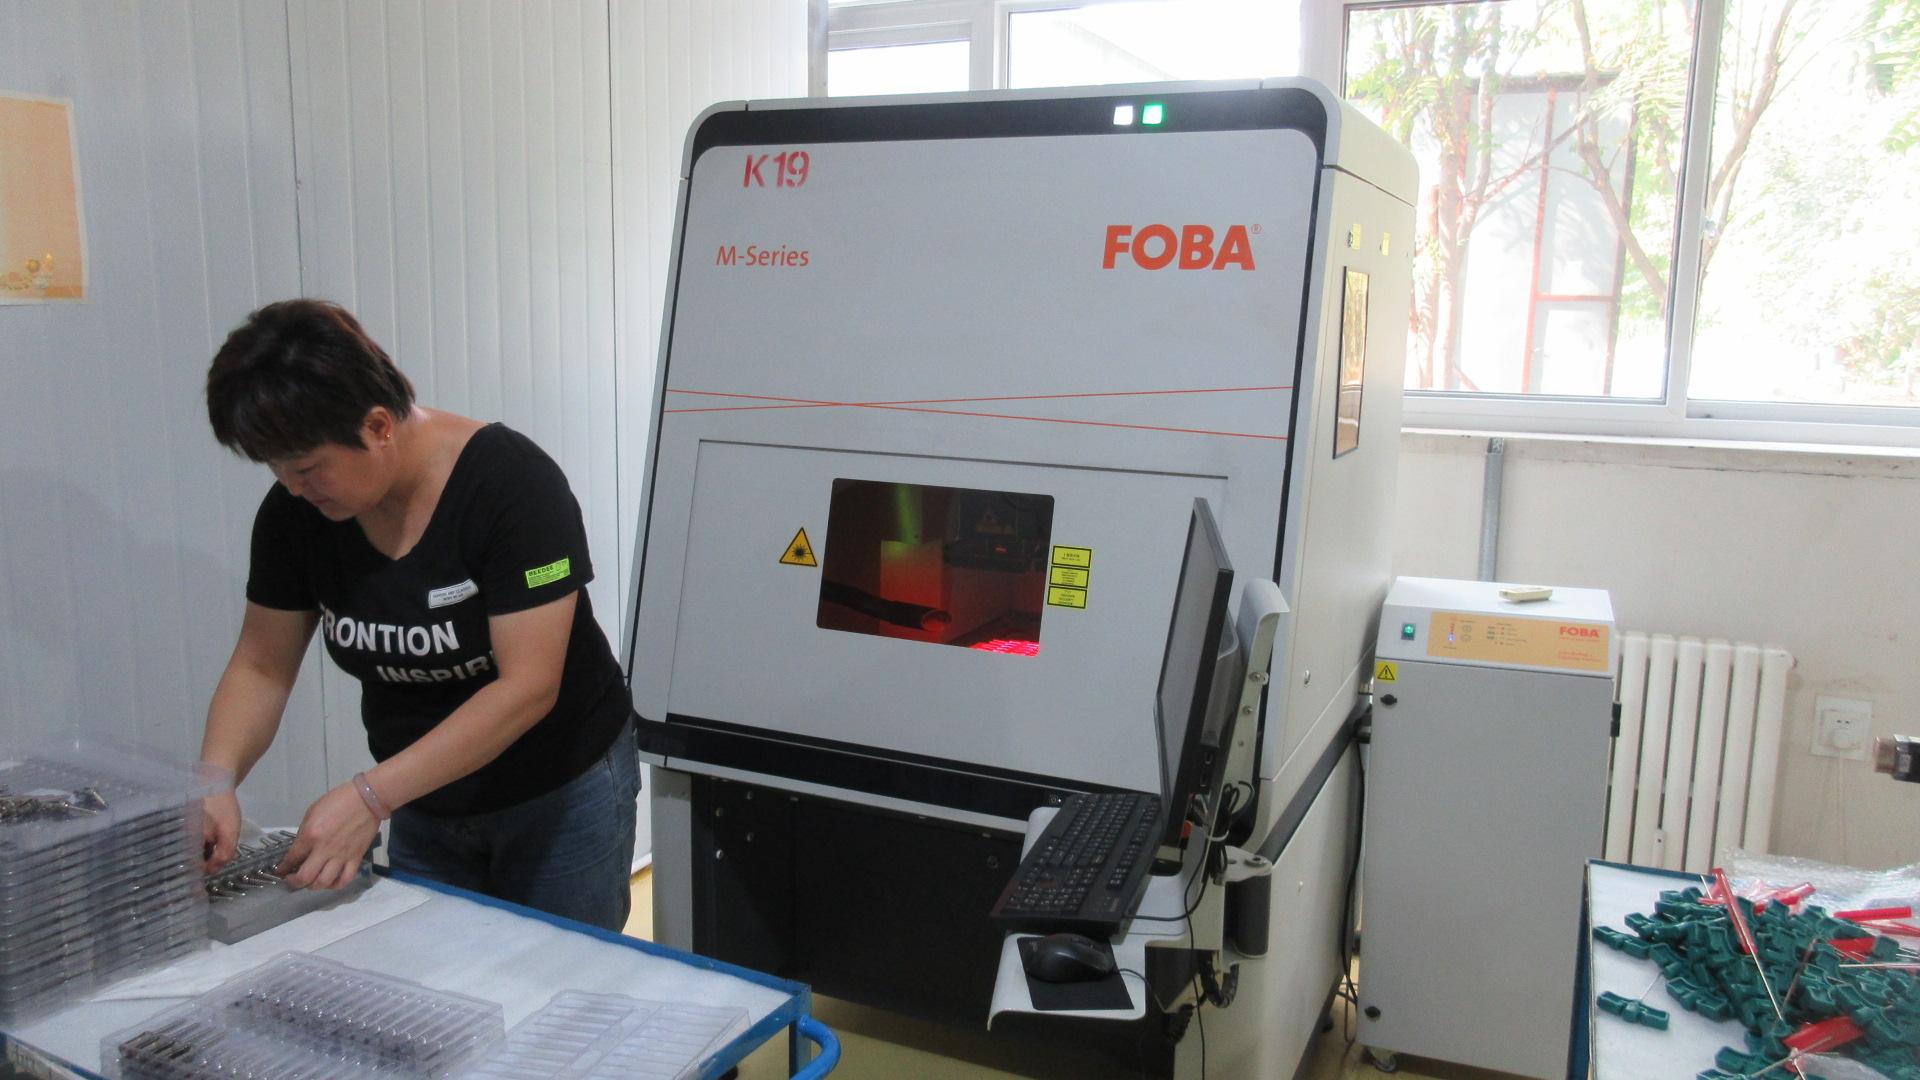
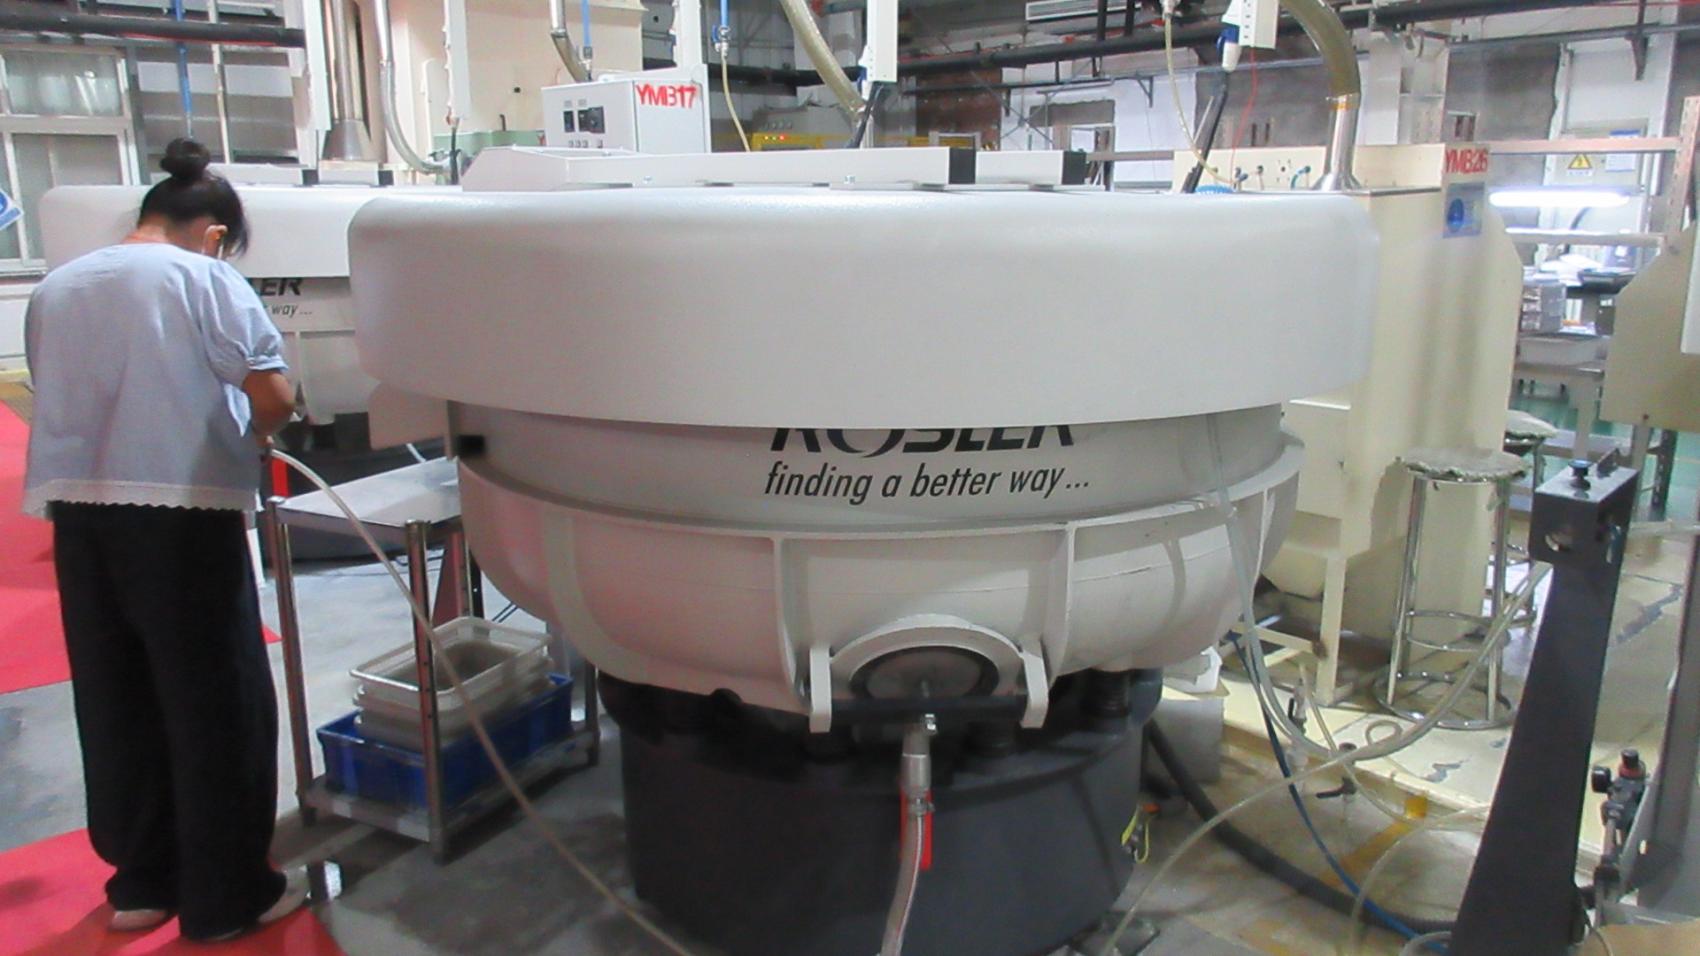
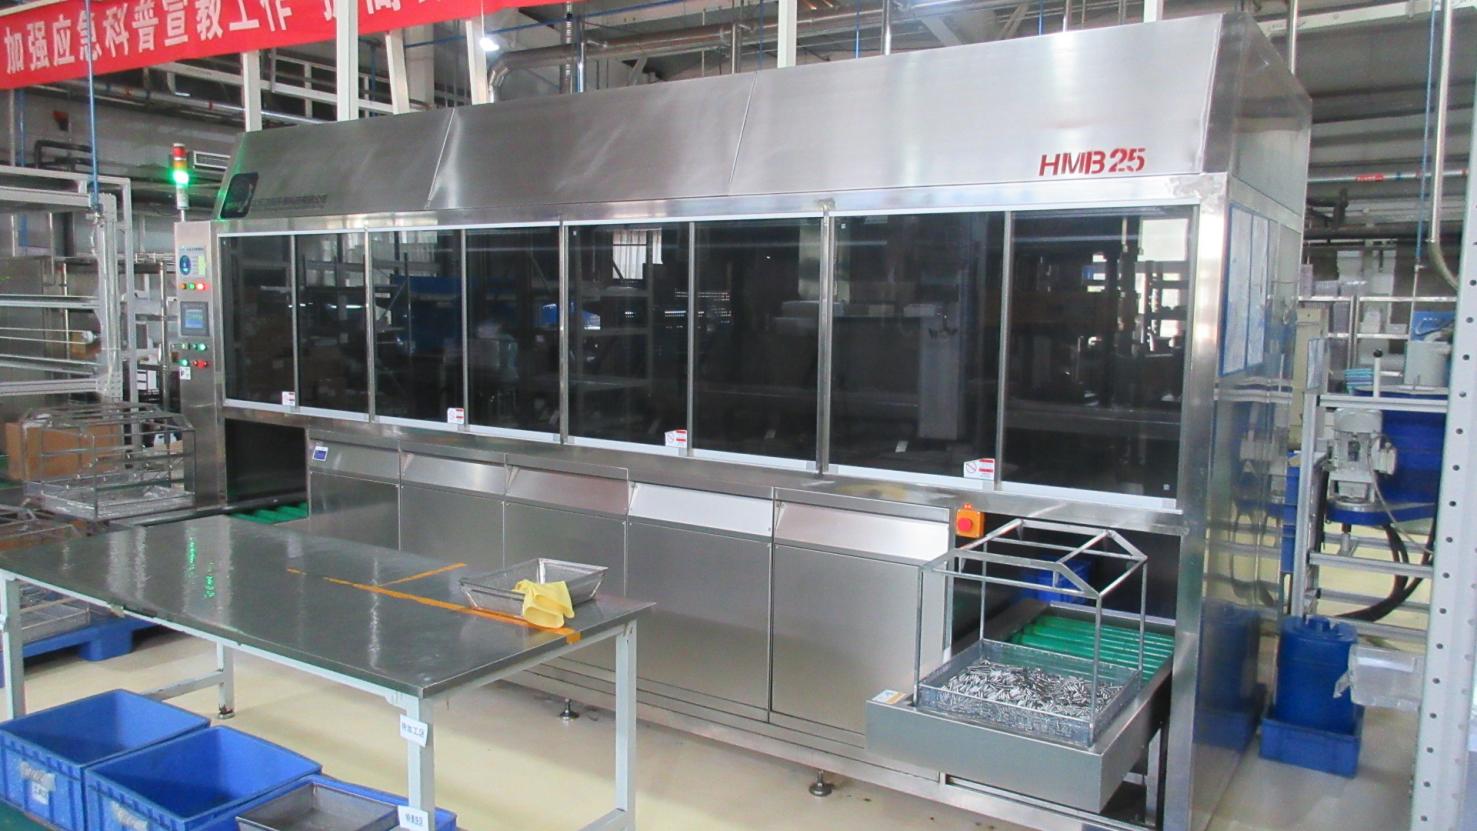
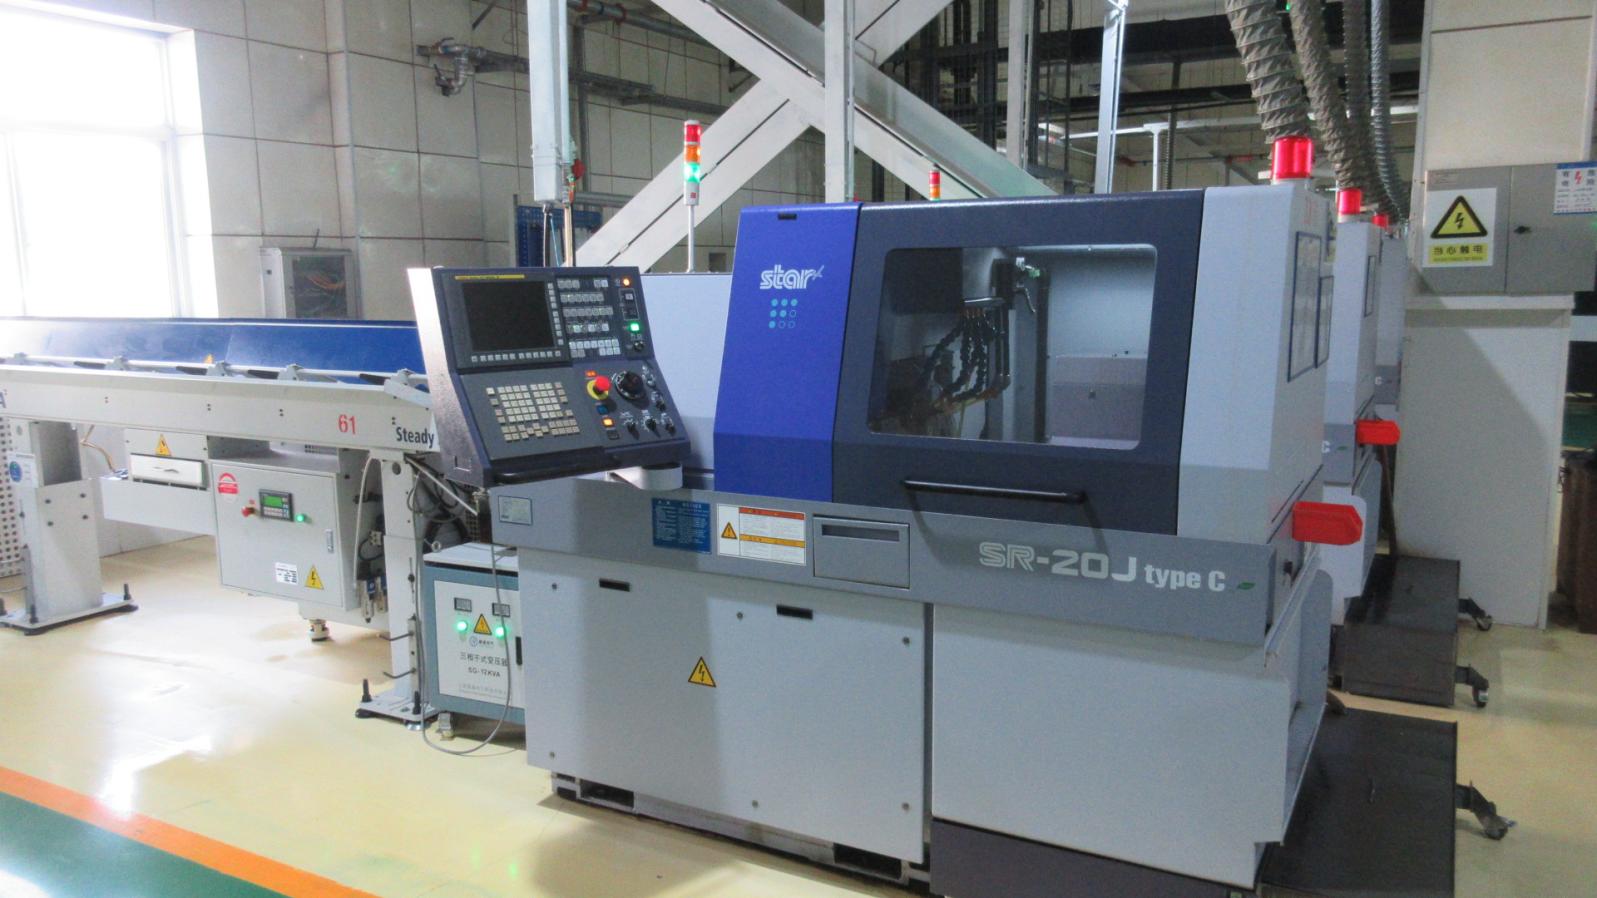
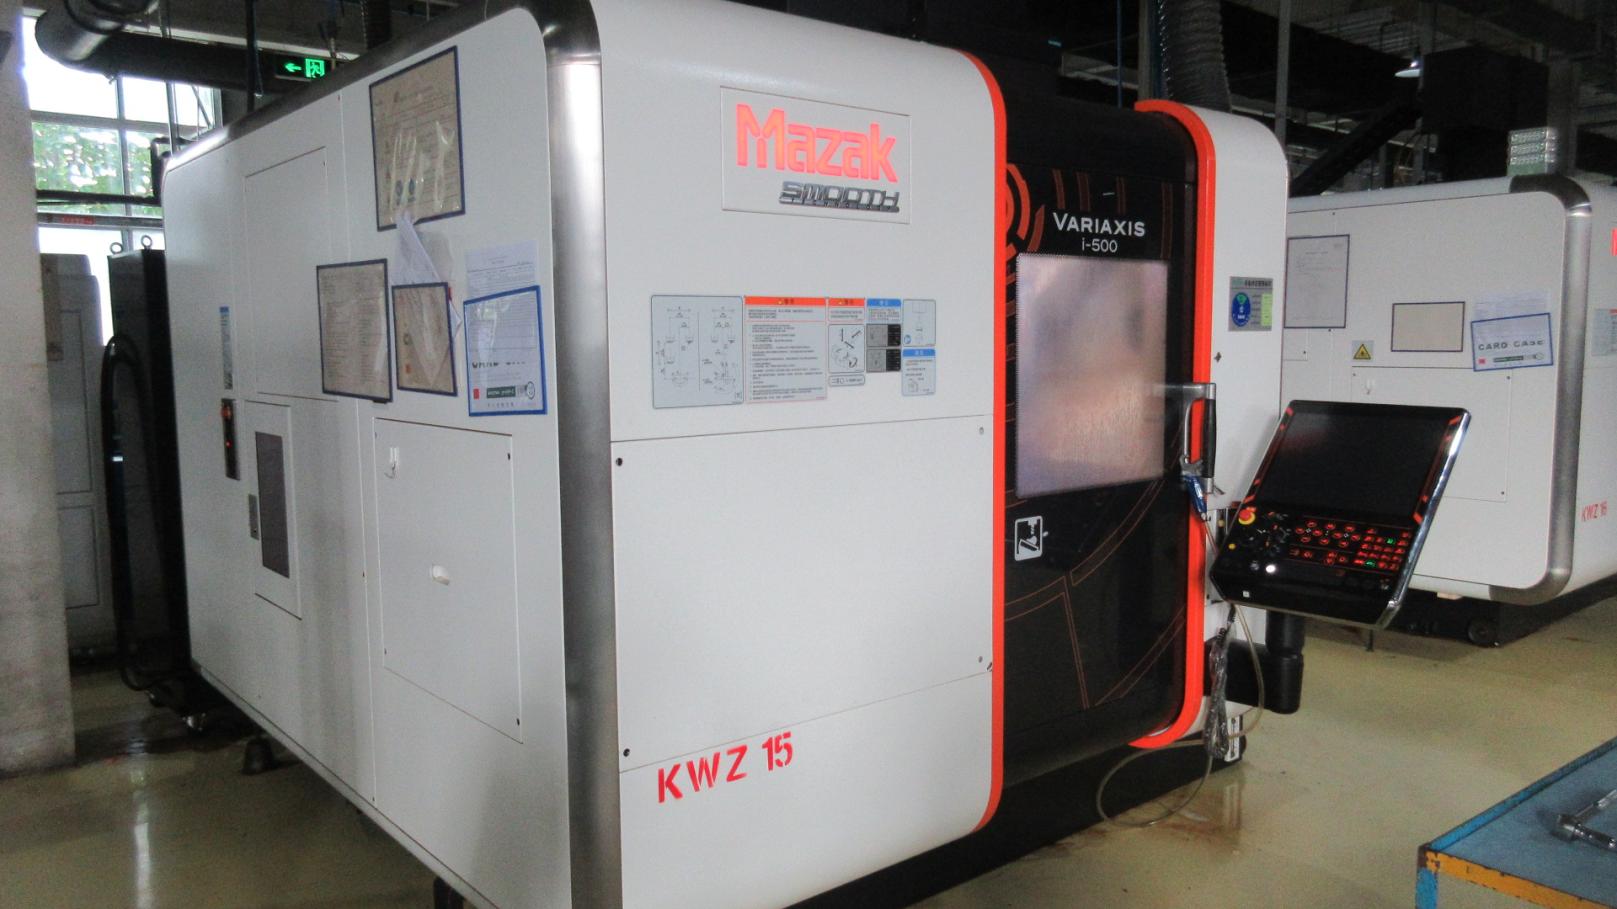
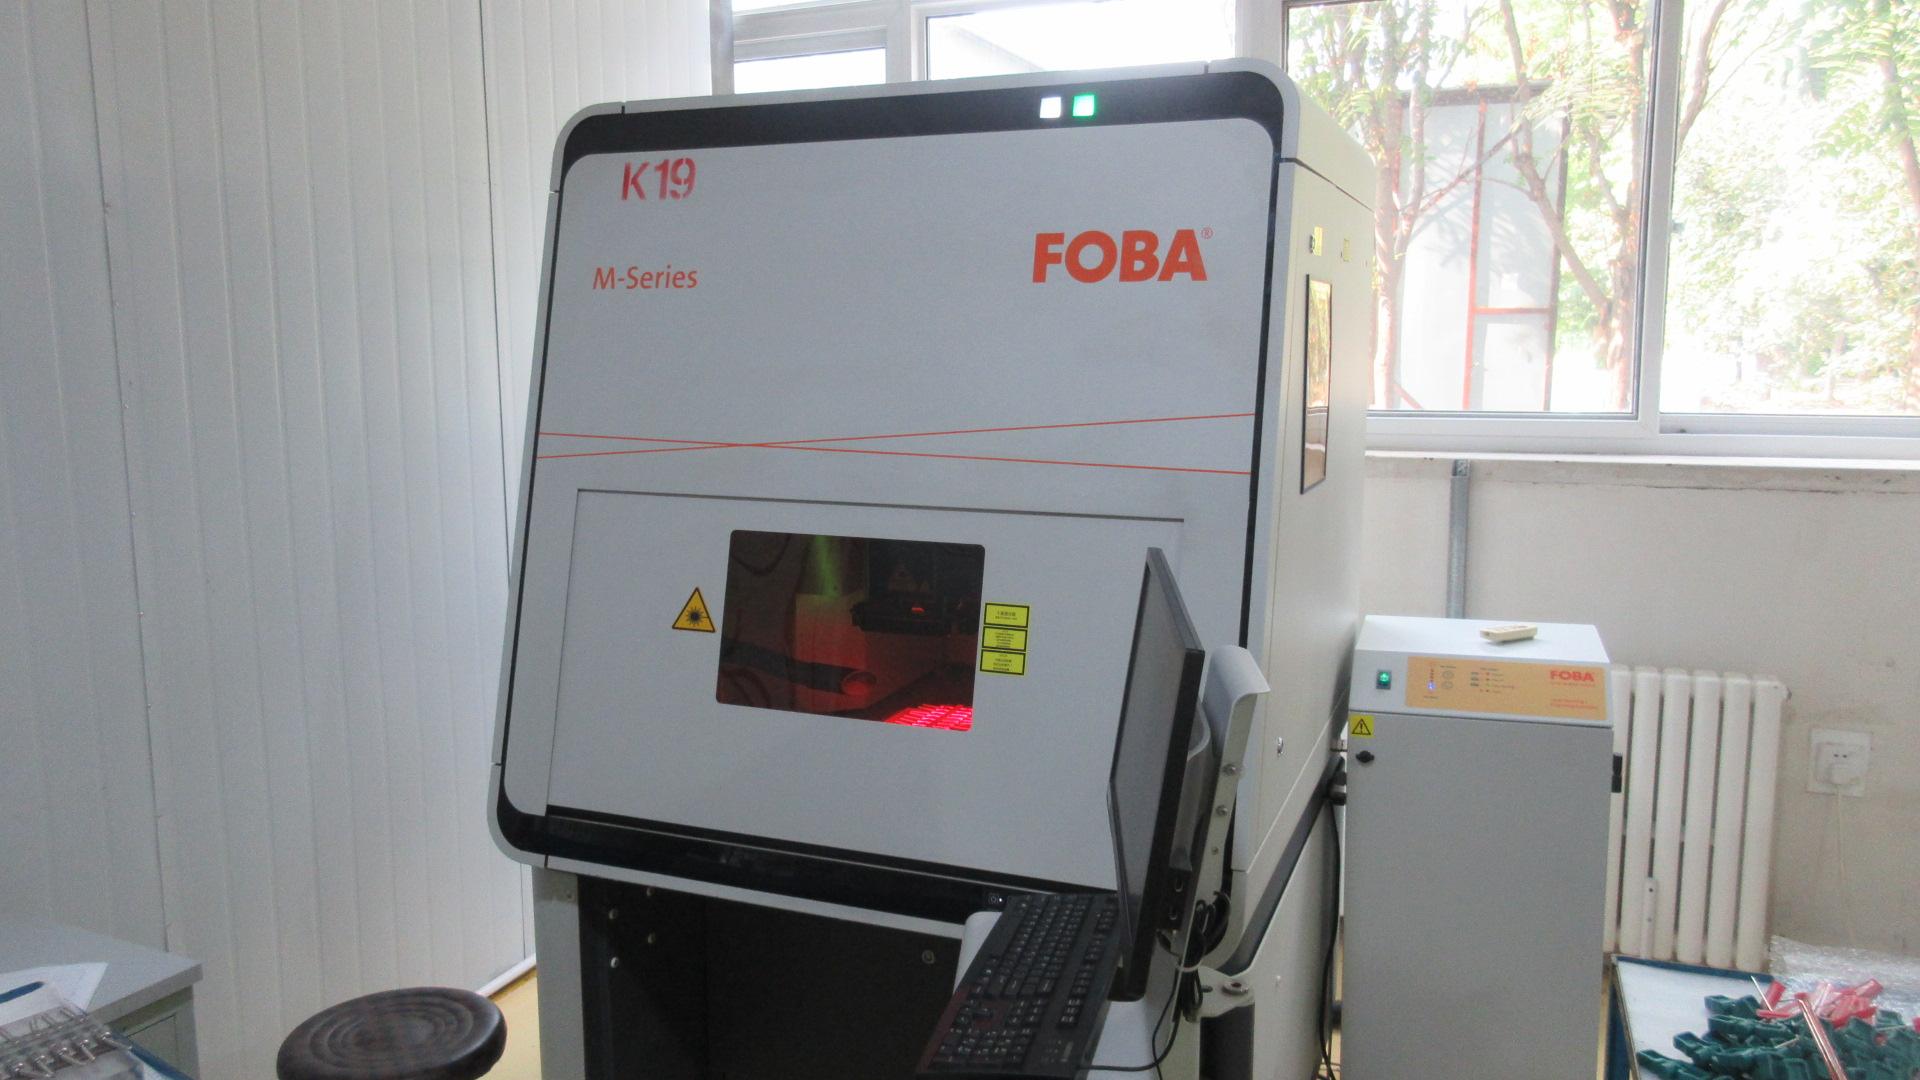
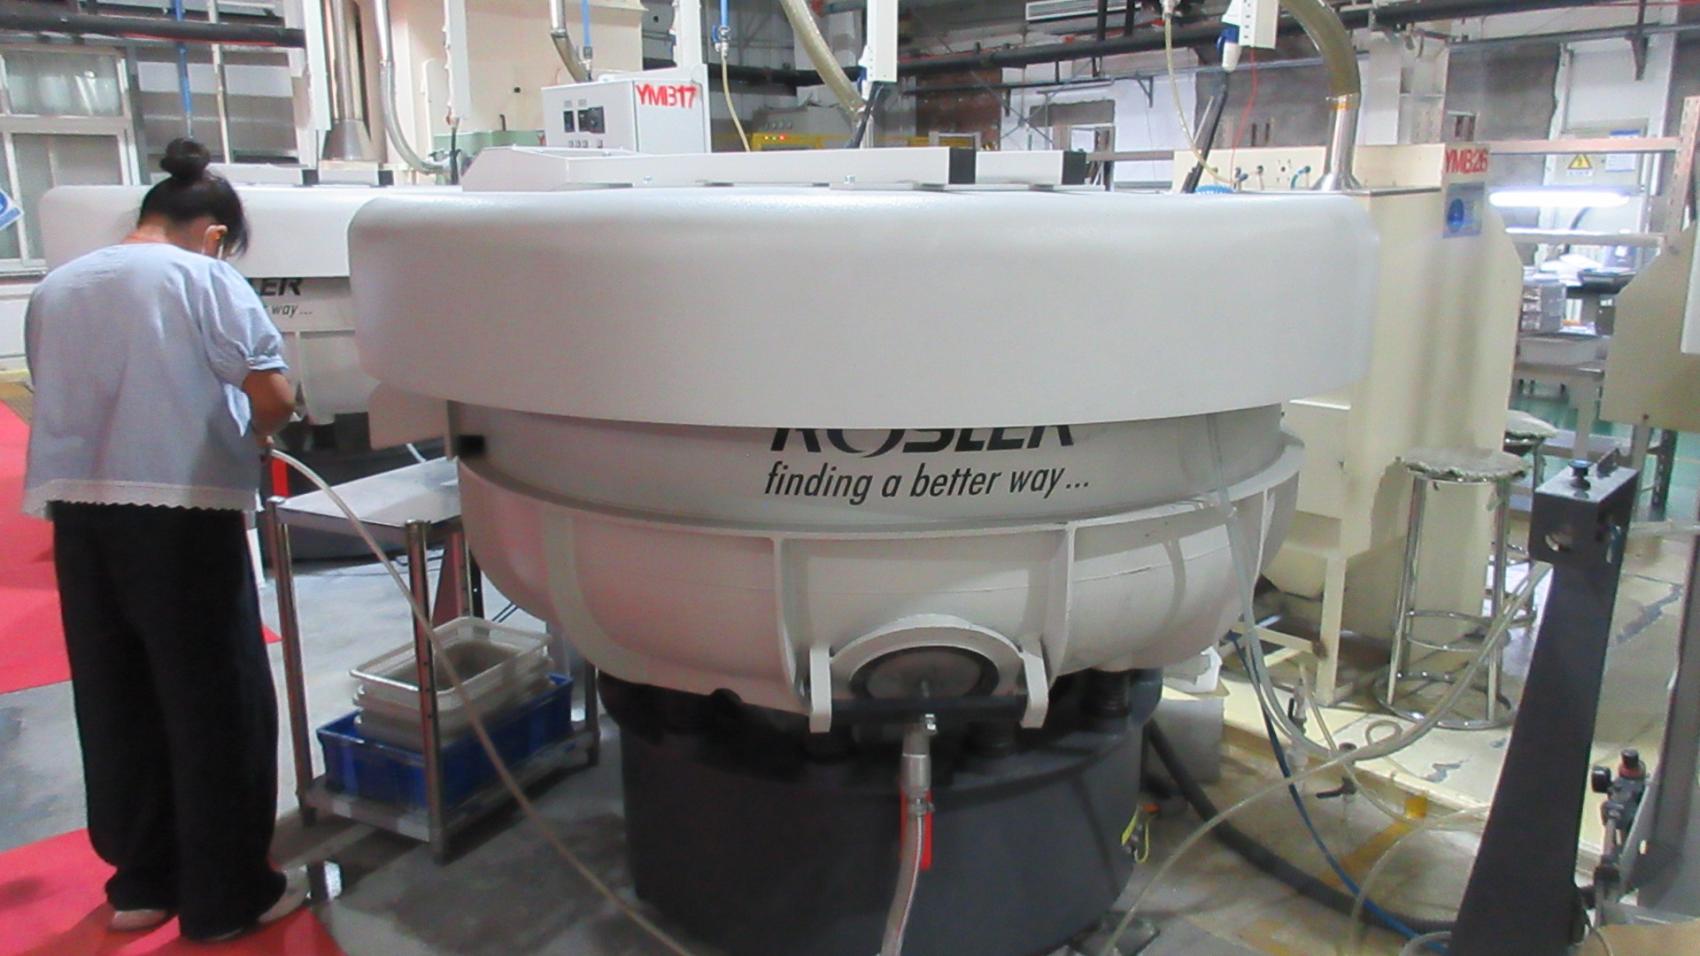
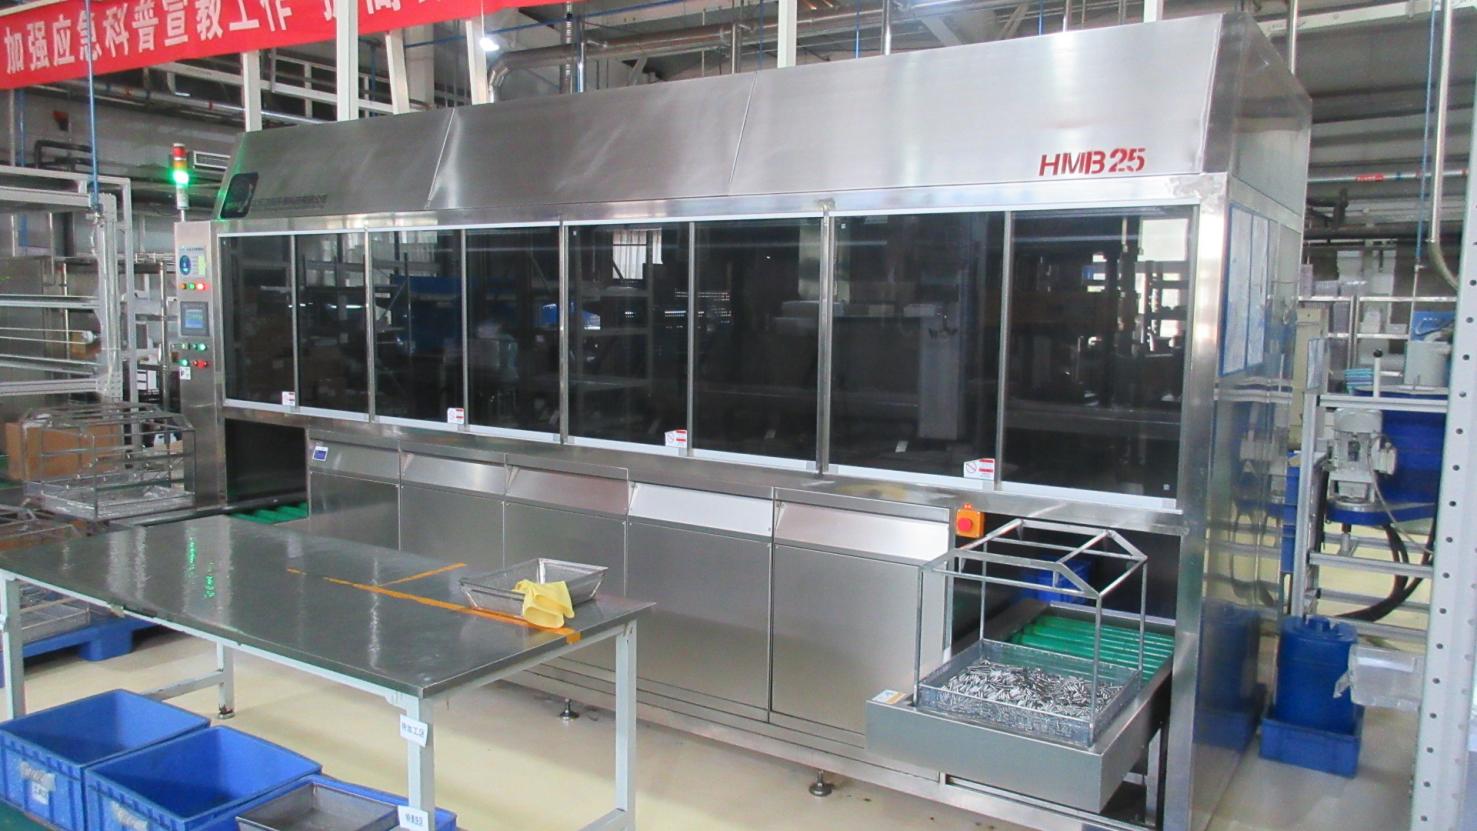
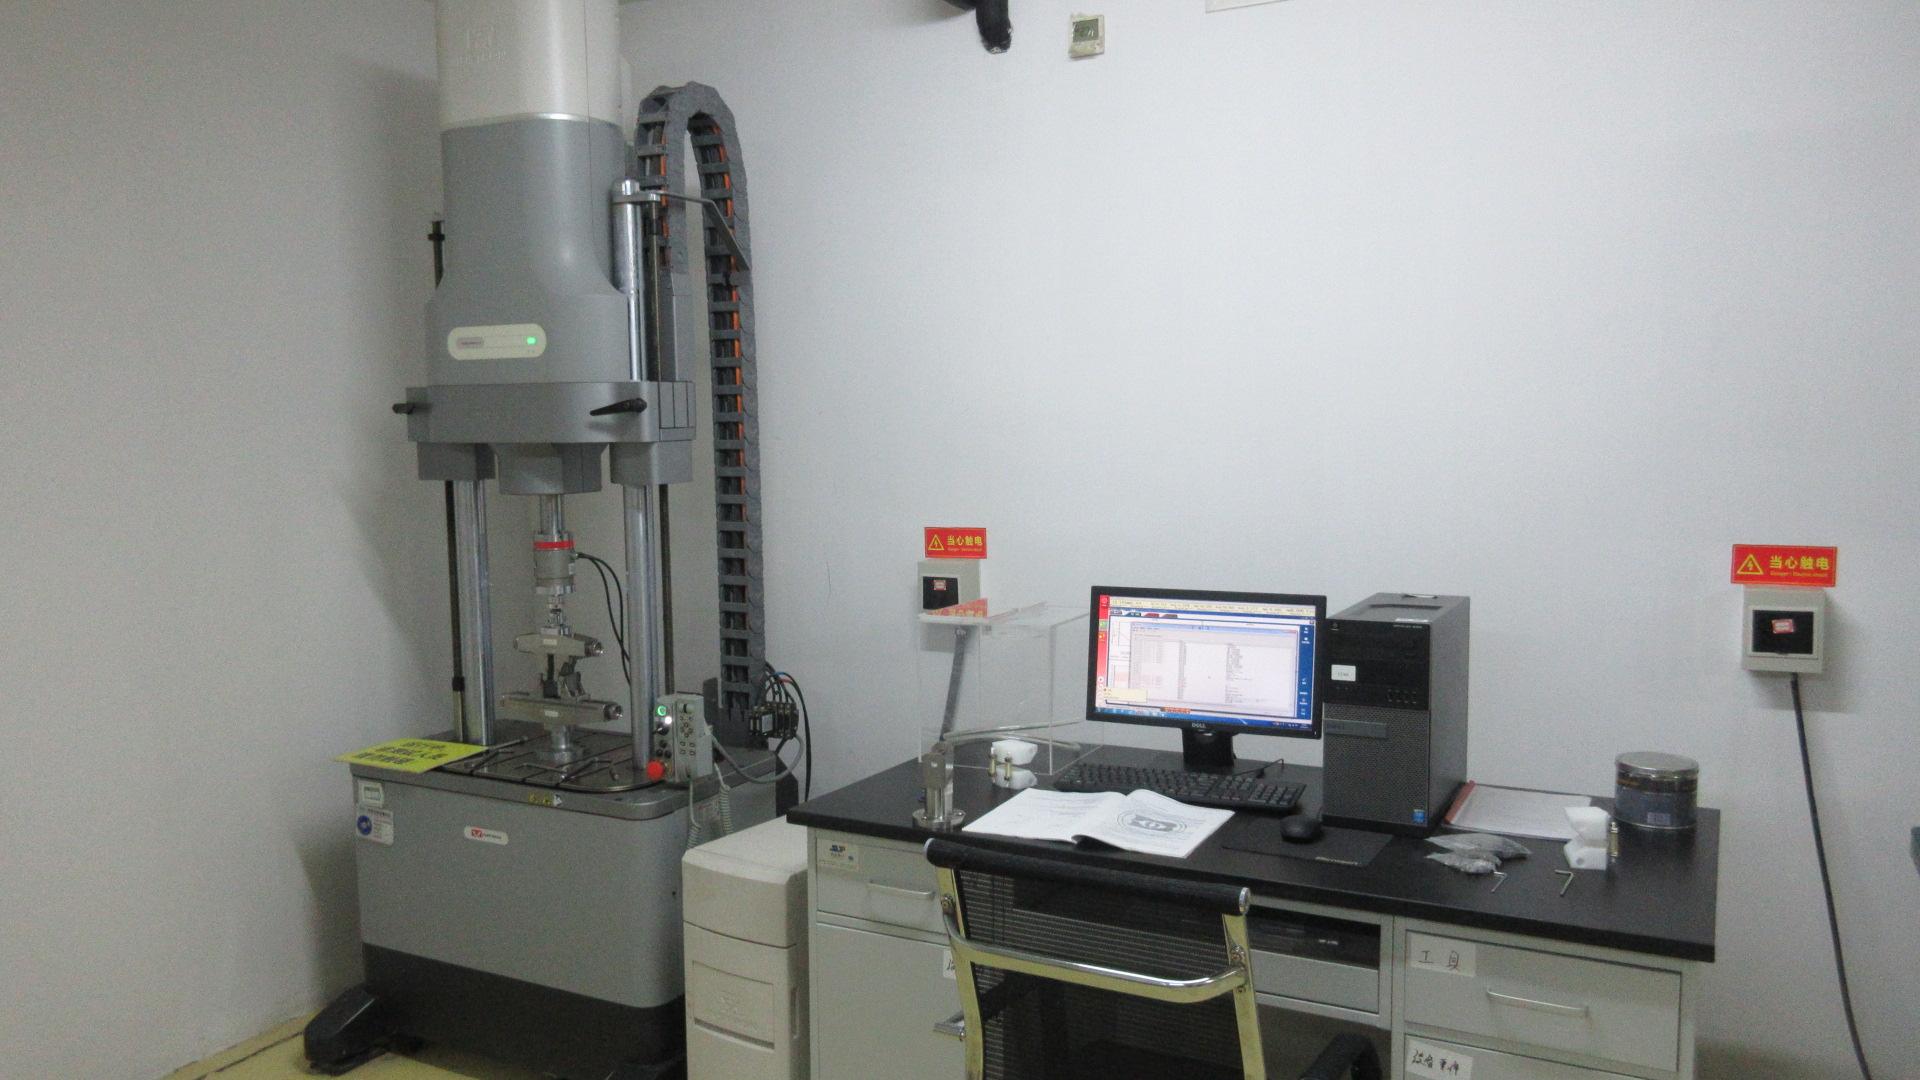
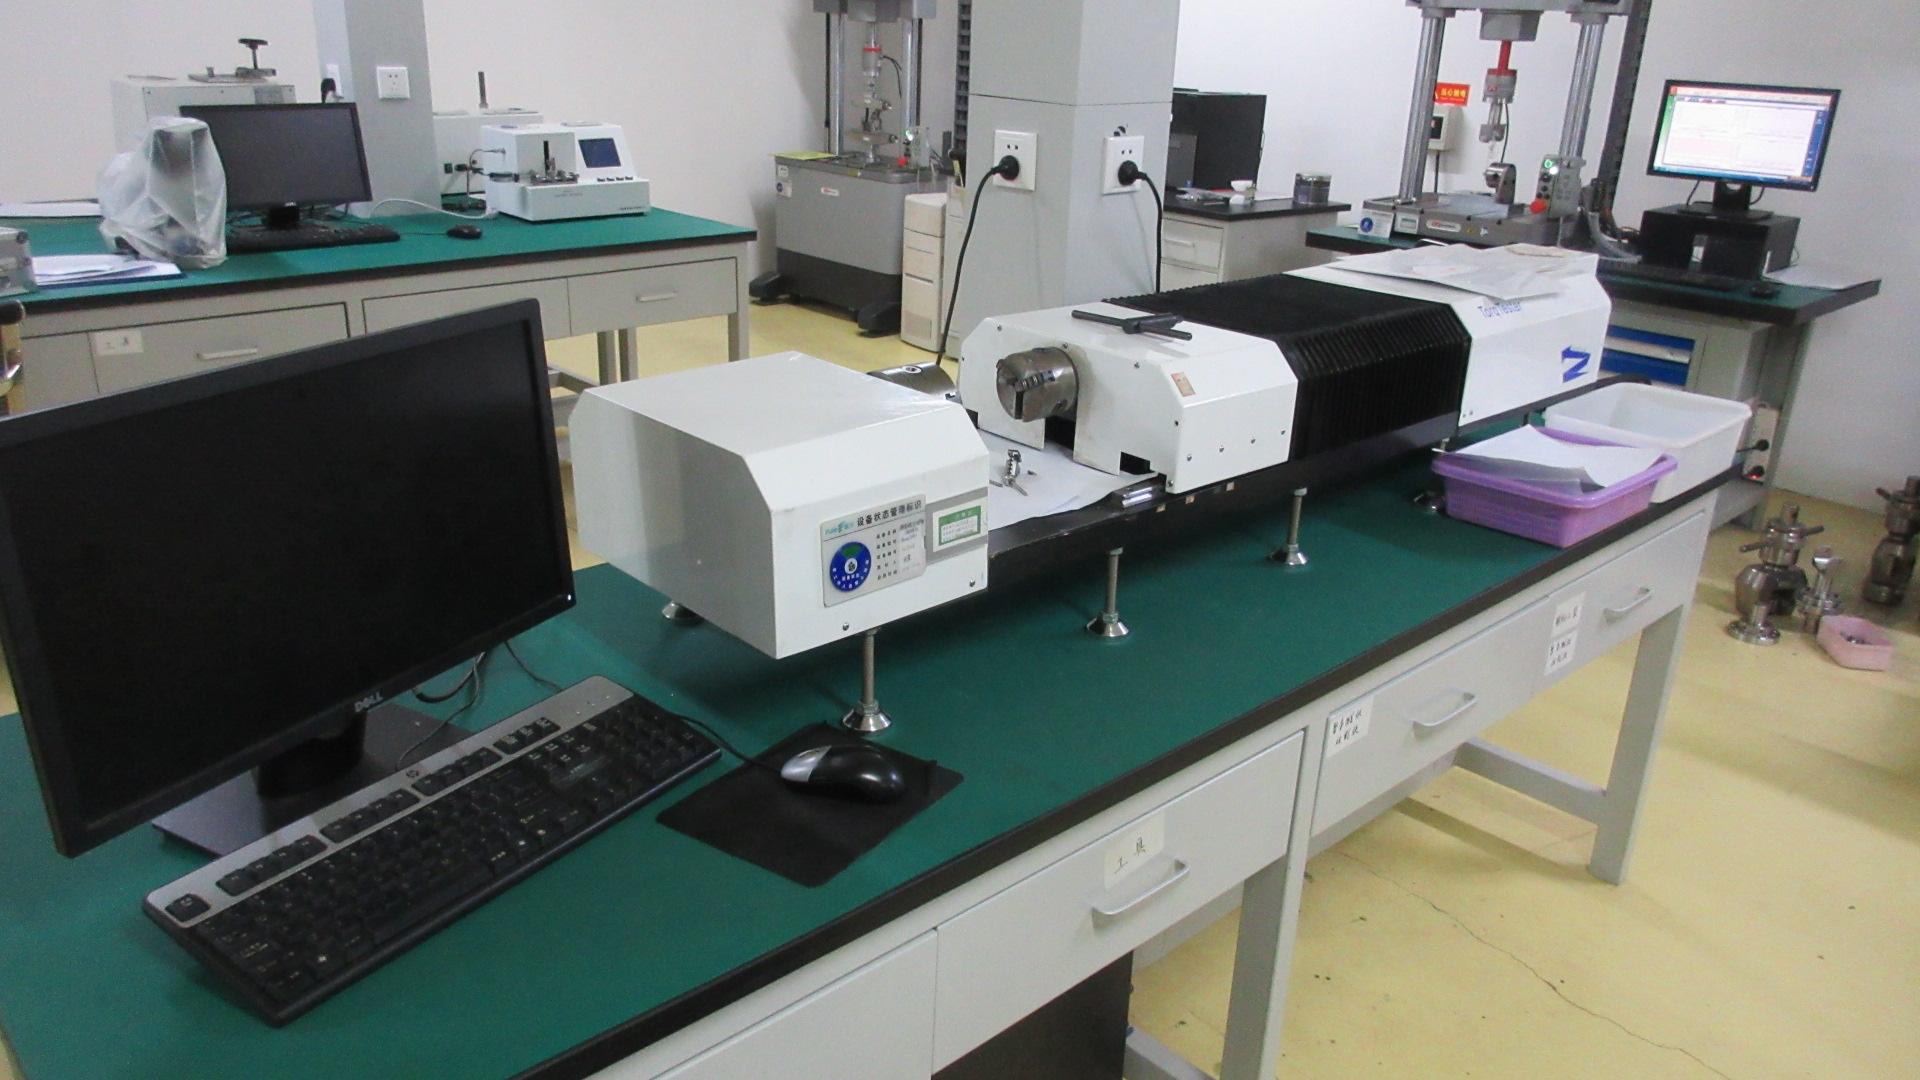
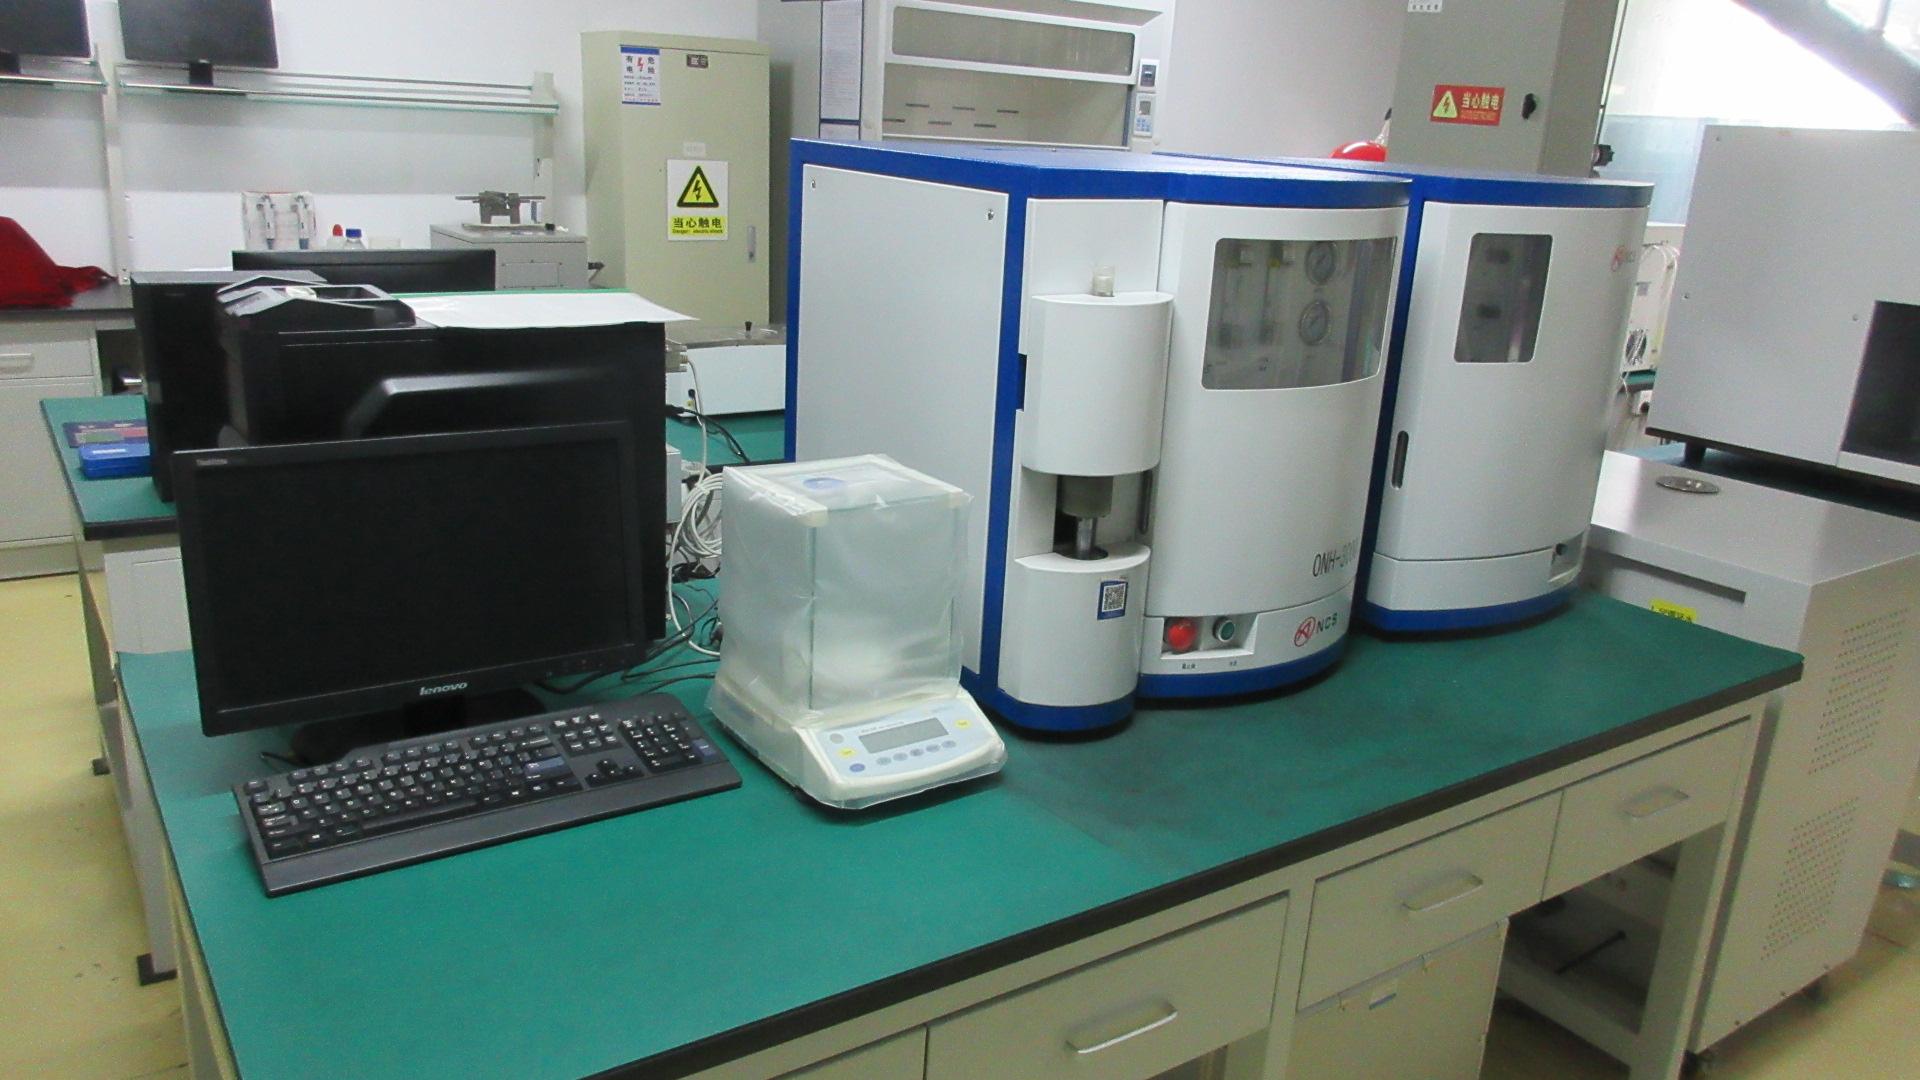
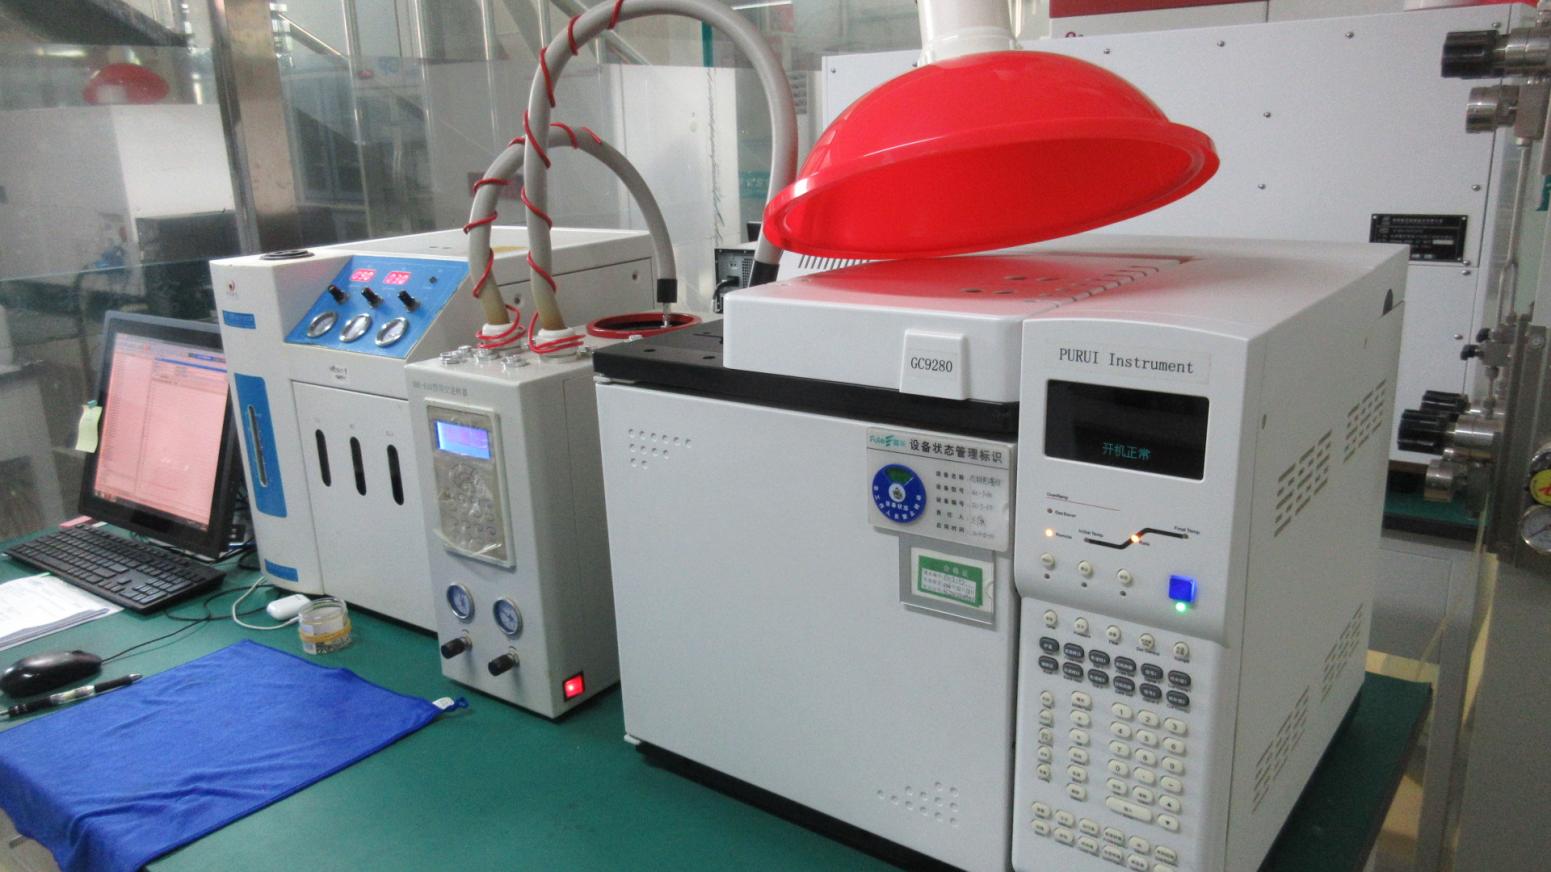
A visual tour of our production environments, quality inspection labs, and high-precision machinery.
Expert answers regarding international shipping, customization options, and regulatory certifications for global healthcare partners.
Our entire product lineup is backed by rigorous international compliance standards, including ISO13485 quality management certifications and CE markings for Class II and Class III medical devices. This ensures seamless customs clearance and regulatory approval across European, Southeast Asian, and domestic markets.
Yes. With an advanced R&D department consisting of 20 seasoned engineers (including 15 graduate specialists), we specialize in sample processing, graphic processing, and on-demand custom implant manufacturing tailored to specific hospital or distributor requirements.
We enforce 100% full-product inspection protocols across our production lines. Backed by 15 dedicated QA/QC inspectors and complete raw material tracking systems, every batch of titanium alloy implants and surgical instruments undergoes rigorous mechanical and biocompatibility testing prior to export.
 Fule